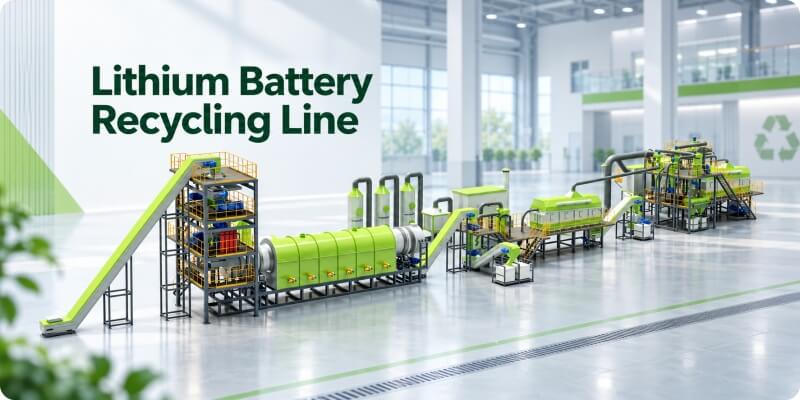
As EV battery retirement accelerates, authorized recovery centers face higher pressure from automakers, regulators and downstream material buyers. Compliance now decides project approval, operating safety and recycling value. A qualified power battery recycling center should connect receiving, traceable storage, scarico, smantellamento, schiacciamento, separazione, dust control and waste gas treatment into one controlled industrial system. This article focuses on how compliance requirements shape equipment selection and plant planning.
How Can Compliance Boundaries Shape A Power Battery Recovery Center Solution?
01 · Compliance BoundariesA power battery recovery center should not choose equipment before confirming its licensed scope. Some centers only collect and transfer batteries. Others dismantle packs or recover black mass. Perciò, the compliance boundary decides the plant layout, safety system, labor plan and investment level.
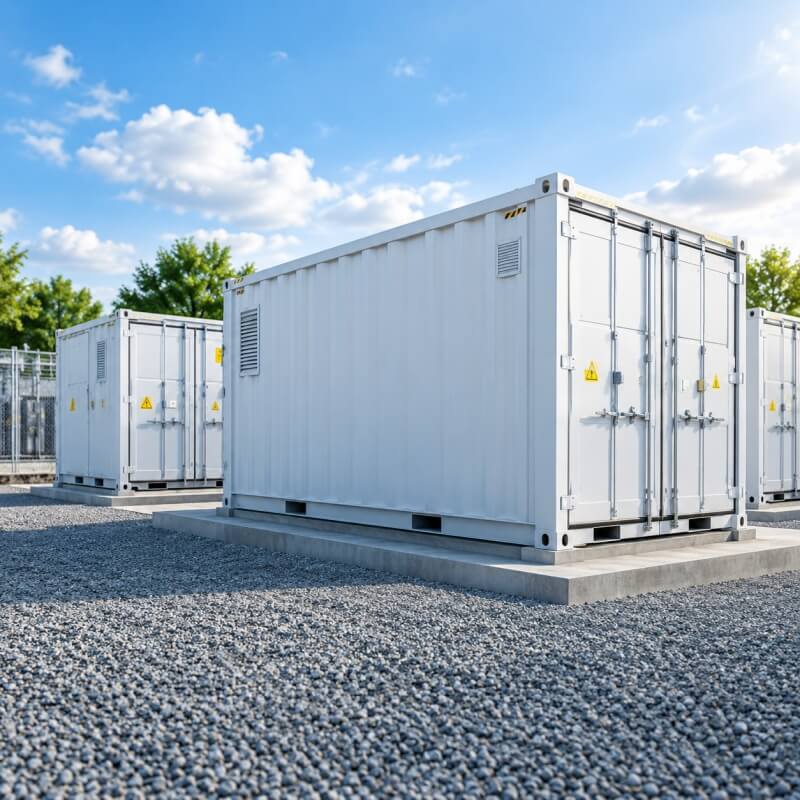
Collection Centers Need Safe Storage
Collection-only centers focus on receiving, testing, magazzinaggio, and transfer. Fire zones, battery records, insulated storage, and emergency areas help ensure safe operation.
Dismantling Centers Need Controlled Handling
Battery dismantling requires insulated tools, attrezzature di sollevamento, testing, and isolation systems. These measures reduce high-voltage risks and improve process traceability.
Recovery Centers Need Complete Recycling Lines
Material recovery centers need discharge, schiacciamento, separazione, controllo delle polveri, and product collection systems. Equipment scale depends on recovery goals and compliance requirements.
How Does Battery Receiving Reduce Compliance Risk Before Storage?
02 · Compliance BoundariesBattery receiving decides the first safety boundary in a power battery recycling center. A damaged pack may carry heat, electrolyte leakage, or residual voltage. So the receiving area needs inspection, classification, isolation and digital records before storage begins.
Incoming Inspection Controls Battery Risk
Batteries should be classified by condition before storage. Ispezione, pesatura, scanning, and isolation zones help control risks before dismantling or crushing.
Traceability Supports Compliance Management
Each battery batch should record source, peso, modello, status, and destination. Complete tracking helps support audits and improves material accountability.
Fire Zoning Protects Storage Safety
Battery storage needs dedicated fire zones, emergency aisles, and monitoring systems. Proper layout protects workers, licenses, and later recycling operations.
How Can A Controlled Discharge And Dismantling Solution Reduce Audit Risk?
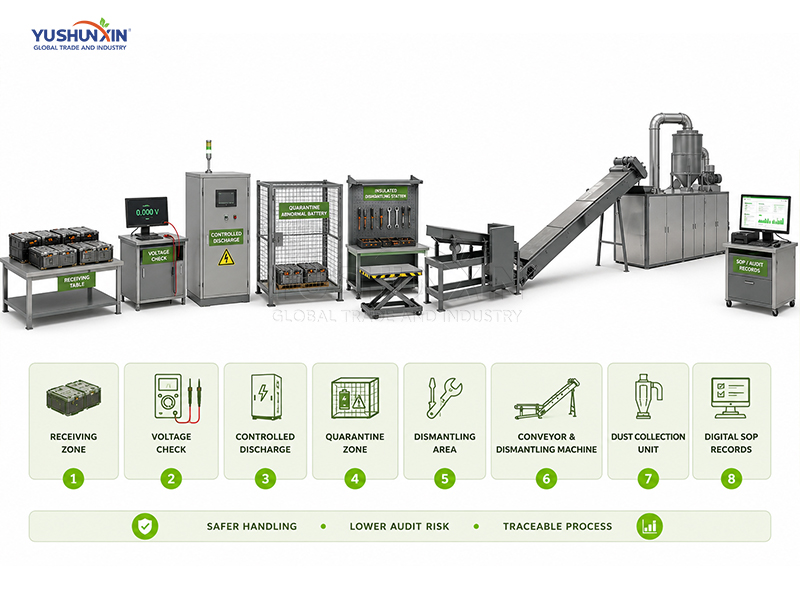
03 · Audit RiskAuthorized recovery centers need stable and repeatable battery handling. Perciò, discharge and dismantling should follow a controlled equipment-based process. This reduces high-voltage exposure, fire risk, dust contact and audit uncertainty.
Residual Power Assessment Comes Before Crushing
Before crushing or deep dismantling, operators should check residual power first. They should record voltage, SOC, temperatura, battery type and abnormal conditions. This step helps classify normal packs, damaged packs and high-risk packs. For compliance projects, salt-water discharge cannot support stable industrial management. It also creates wastewater, corrosion and difficult process control. Perciò, high-voltage batteries should use professional discharge equipment. An industrial discharge system can control discharge time and final voltage. It can also connect records with batch numbers. Di conseguenza, the plant gains safer operation and clearer audit evidence.
Industrial Pack Dismantling Limits Worker Exposure
Battery pack dismantling should reduce direct manual contact. The line can include lifting platforms, insulated worktables and pneumatic tools. It can also add dust collection and module dismantling fixtures. These configurations make pack opening more stable. They also reduce contact with high-voltage parts, electrolyte residue and metal dust. COSÌ, the dismantling area becomes safer and easier to manage. For large authorized centers, this design also improves labor efficiency. Workers handle packs by process steps, not personal experience. This helps the center maintain stable daily throughput.
Digital SOP Records Make Compliance Review Easier
Complete operation records help prove safe battery handling. Key data includes discharge, smantellamento, ispezione, manutenzione, and training records. A digital SOP system supports audits, improves management, and strengthens recycling compliance.
Ottieni la tua soluzione!How Should A Closed Crushing-Separation Line Secure Material Accountability?
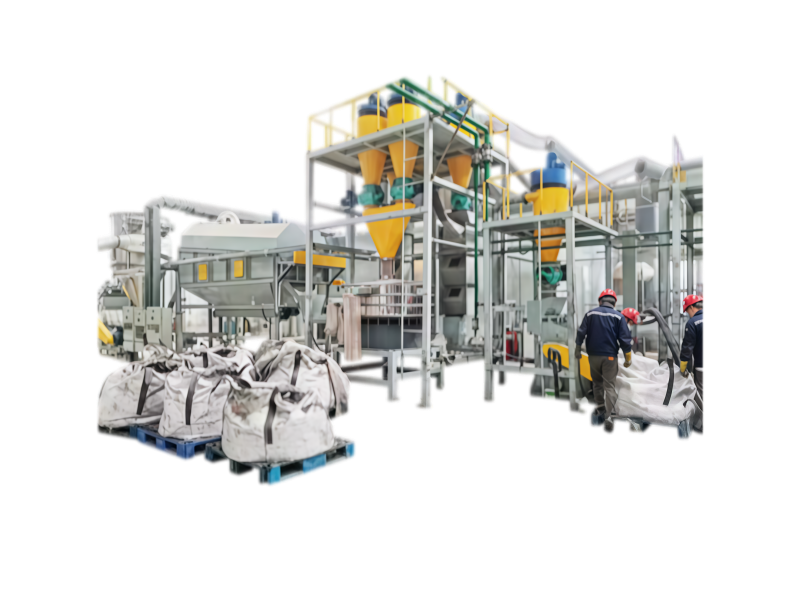
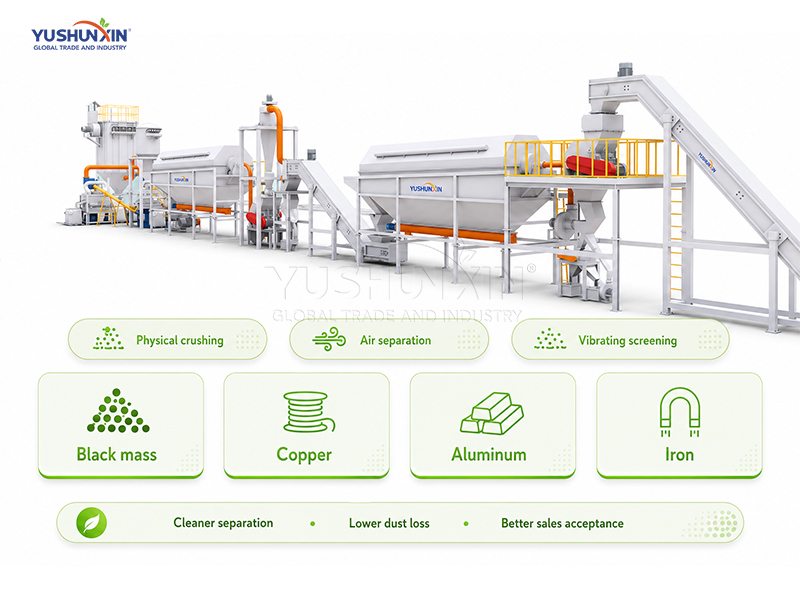
04 · Material AccountabilityAfter discharge and dismantling, material accountability becomes the project’s core value. The line should turn mixed battery materials into traceable outputs. Perciò, alimentazione, schiacciamento, separazione dell'aria, screening and collection must work together. A compliant recovery center should know how much black mass, rame, aluminum and iron leaves each production batch.
Controlled Feeding Stabilizes The Crushing Section
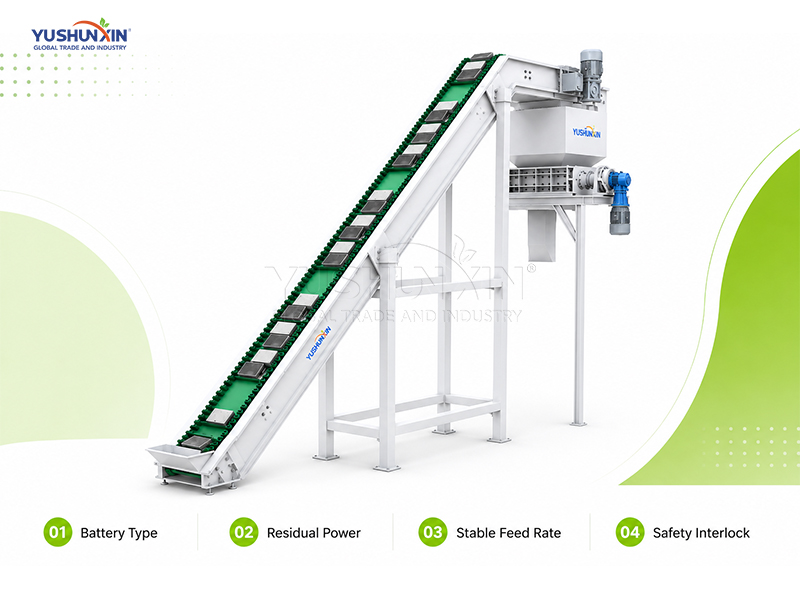
Before crushing, the operator should confirm battery type, misurare, residual power and impurity level. This step protects the crusher and reduces abnormal shutdowns. The feeding system can include belt conveyors, sealed hoppers, metering feeders and safety interlocks. These units help the line feed batteries at a stable rate. Nel frattempo, they reduce dust leakage and operator exposure. For authorized recovery centers, stable feeding matters more than crusher power alone. It helps keep production records clear. It also supports safer batch management.
Physical Separation Turns Mixed Materials Into Saleable Outputs
A power battery recycling line can use physical crushing as the core process. Poi, air separation and vibrating screening classify different materials. This process can separate black mass, rame, alluminio e ferro. Di conseguenza, the recovery center can improve product classification. It can also provide clearer data for downstream buyers. Black mass quality depends on impurity control. Perciò, the separation system should reduce metal mixing and dust loss. Better classification often means better sales acceptance.
Licensed Throughput Should Decide The Line Capacity
Capacity planning should not focus on one crusher only. The buyer should review the complete line capacity. This includes feeding speed, crushing output, screening efficiency and dust collection capacity. Per esempio, 500kg/h and 1000kg/h lines can serve different project stages. A 500kg/h line may suit pilot or regional centers. A 1000kg/h line suits larger authorized recovery networks. Tuttavia, capacity must match the license, warehouse volume and working hours. It should also match downstream black mass and metal buyers. Altrimenti, the plant may create storage pressure after production.
How Can A Closed Environmental Control Plan Secure The Power Battery Recycling Line?
05 · Control PlanEnvironmental control should follow the material flow. It should not start after crushing. A power battery recycling line produces messa nera, metal particles, dust and process gas. Perciò, the plant needs sealed collection, negative-pressure transfer, dust filtration, gas treatment and residue classification. Per progetti industriali, the environmental system should match real capacity, such as 500kg/h or 1000kg/h recycling lines.
MASS QUALITY
Seal Dust Points For Black Mass Quality
Frantumazione, screening, trasporto, and discharge points should use sealed designs. Negative pressure and dust collectors reduce powder loss and improve black mass quality.
GAS
Treat Gas Before Workshop Release
Battery processing may create odor, polvere, and volatile gas. Source collection, filtrazione, assorbimento, and exhaust systems help protect workers and support compliance.
RESIDUI
Manage Residues With Clear Routes
Non-recyclable residues need classified storage and qualified disposal channels. Proper residue management reduces compliance risks and protects product value.
How Can A Compliance-Based Recycling Solution Improve Project ROI?
06 · ROI
Compliance should not only appear in approval documents. It should enter the full recycling solution. For authorized recovery centers, ROI comes from stable throughput, cleaner black mass, lower labor cost and stronger downstream acceptance. Perciò, the plant should combine safe operation, product control and audit-ready documents from the beginning.
Product Quality Improves Black Mass Value
Black mass value depends on purity, umidità, and batch stability. Stable crushing, separazione, and sealed collection help reduce impurities and improve buyer acceptance.
Automation Reduces Operating Loss
Long-term operation depends on stable automation. Alimentazione automatica, separazione, and dust control reduce labor demand, downtime, and daily operating risks.
Documents Support Project Approval
Industrial projects need complete technical documents for approval and financing. Flusso del processo, layout, manuali, and training records help improve project credibility.
Riepilogo
Power battery recycling compliance should guide the whole recovery center plan. A qualified project should connect receiving, traceability, safe storage, scarico, smantellamento, schiacciamento, separazione, controllo delle polveri, waste gas treatment and product collection. Perciò, investors need more than single equipment. They need a complete recycling solution that supports approval, operation and material sales. Yushunxin can provide a customized power battery recycling solution based on battery type, capacità, disposizione del sito, compliance needs and product target. Our solution can include process design, configurazione dell'apparecchiatura, disposizione degli impianti, controllo ambientale, guida all'installazione, commissioning and technical training. And if you also want to get impianto di riciclaggio delle batterie al litio, Ess battery recycling line E EV battery disposal plan, per favore contattaci.
Dalle tue esigenze
all'impatto reale


