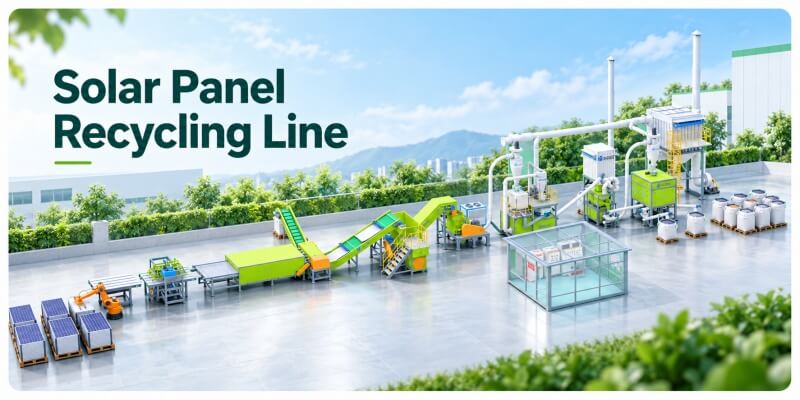
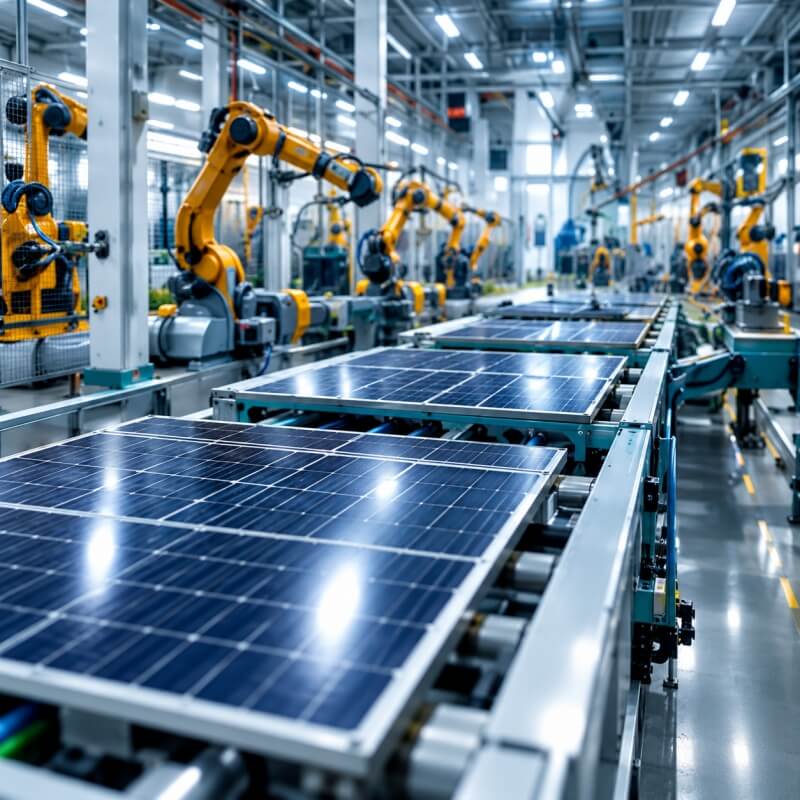
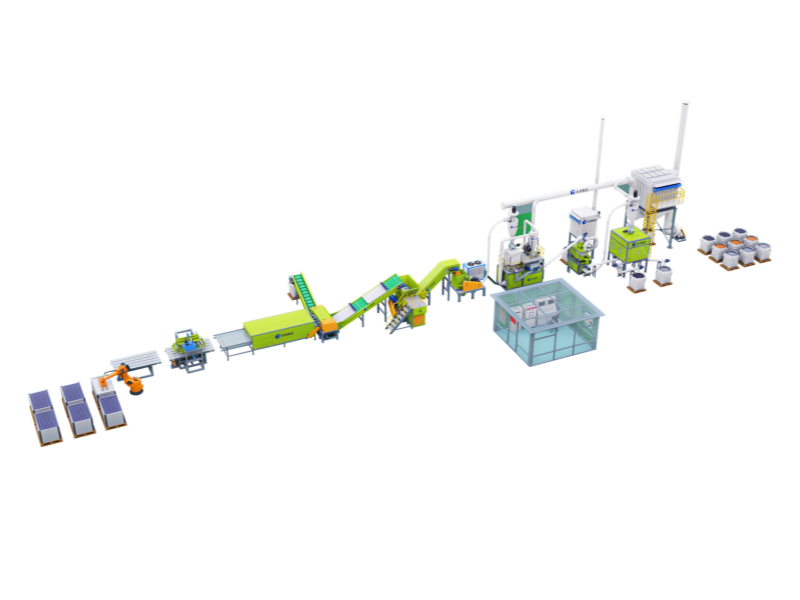
Establishing an industrial photovoltaic recycling plant requires an end-to-end operational solution. Por lo tanto, successful recyclers look beyond individual equipment to build high-efficiency recovery lines. Our solar panel recycling machines streamline single-glass and double-glass module processing. Mientras tanto, integrated thermal and mechanical units maximize pure glass, silicio, and precious silver recovery. Además, optimized plant layouts lower daily energy costs while maintaining strict environmental compliance. In short, this solution helps B2B investors minimize initial capital risk, accelerate project setup, and secure continuous profitability from retired solar panels.
How to Align Feedstock Types With Your Industrial Recycling Capacity?
01 · Materia primaIndustrial recycling plants must categorize incoming photovoltaic feedstocks before equipment selection. Different module structures dictate distinct processing routes and throughput capacities. Por lo tanto, mapping your material sources directly to the correct recycling system prevents operational bottlenecks and secures high material purity.
Single-Glass vs Double-Glass Feedstock Handling
Single-Glass Module Processing
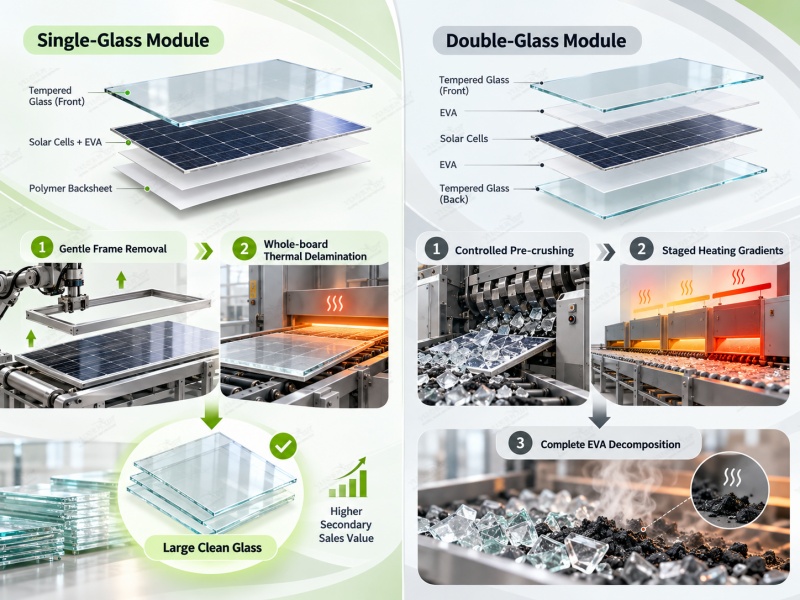
Single-glass panels feature front tempered glass, polymer backsheets, and EVA encapsulation. These panels allow gentle eliminación del marco and whole-board thermal delamination. Como consecuencia, this route protects large clean glass pieces and maximizes secondary sales value.
Double-Glass Module Processing
Double-glass modules contain dual glass layers without organic backsheets. Por lo tanto, they require controlled pre-crushing or specialized staged heating gradients. Proper thermal management prevents glass thermal shock and ensures complete EVA decomposition.
Feedstock Contamination and Preprocessing Standards
Batch Inspection and Sorting
Incoming retired panels often exhibit frame corrosion, broken corners, or attached junction boxes. Operators must inspect and sort incoming batches rigorously. Automated frame and junction box removal units eliminate heavy metal contamination.
Stabilizing Processing Performance
Standardized sorting removes foreign impurities effectively. Además, strict cleaning standards stabilize crusher performance and protect downstream sorting efficiency.
What Are the Core Mechanical and Thermal Processing Solutions for High Recovery?
02 · SolucionesIndustrial e-waste recyclers require an integrated processing route that combines automated mechanical breaking with controlled thermal decomposition. Por lo tanto, our engineered system bridges front-end dismantling with deep thermal liberation to maximize material purity. Mientras tanto, advanced equipment configurations protect valuable glass and metal components from excessive mechanical damage. Como consecuencia, industrial clients achieve stable 7×24 hour continuous operations with exceptional recovery yields.
Mechanical Size Reduction and Physical Sorting
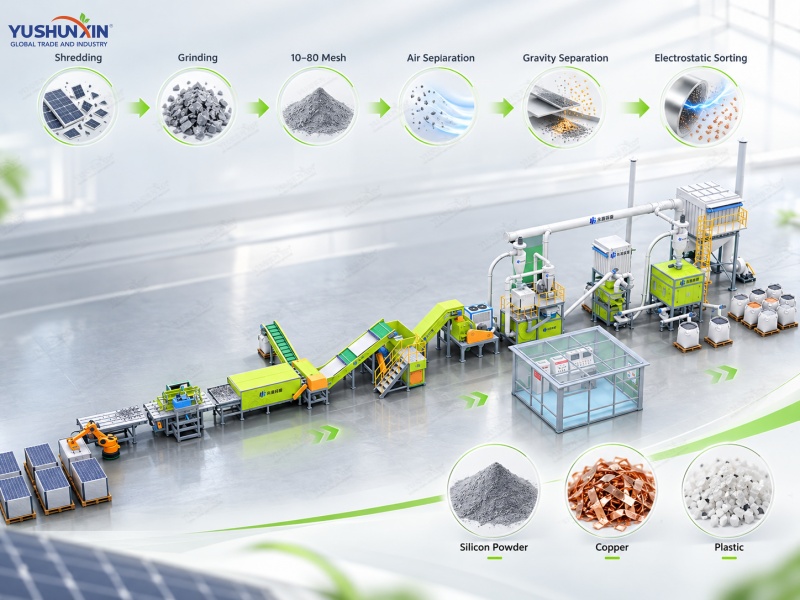
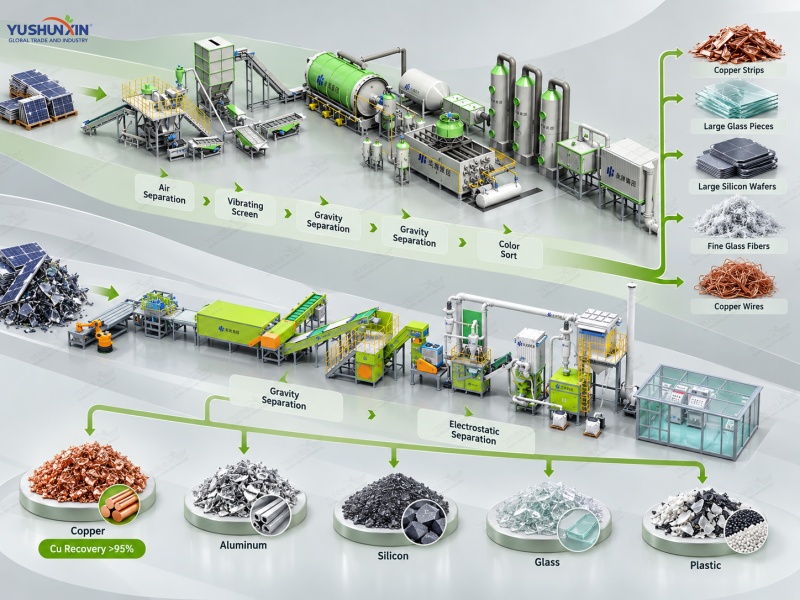
Robust mechanical shredders and hammer crushers break down dismantled panels into manageable fractions. Después, industrial grinders reduce the liberated solid mixtures into fine particles ranging from 10 to 80 malla. Además, specialized air classifiers, separadores de gravedad, y separadores electrostáticos sort the pulverized materials efficiently. Por lo tanto, this multi-stage physical separation route successfully isolates high-purity silicon powders, cintas de cobre, and plastic fractions without chemical contamination.
Thermal Pyrolysis and Controlled EVA Release
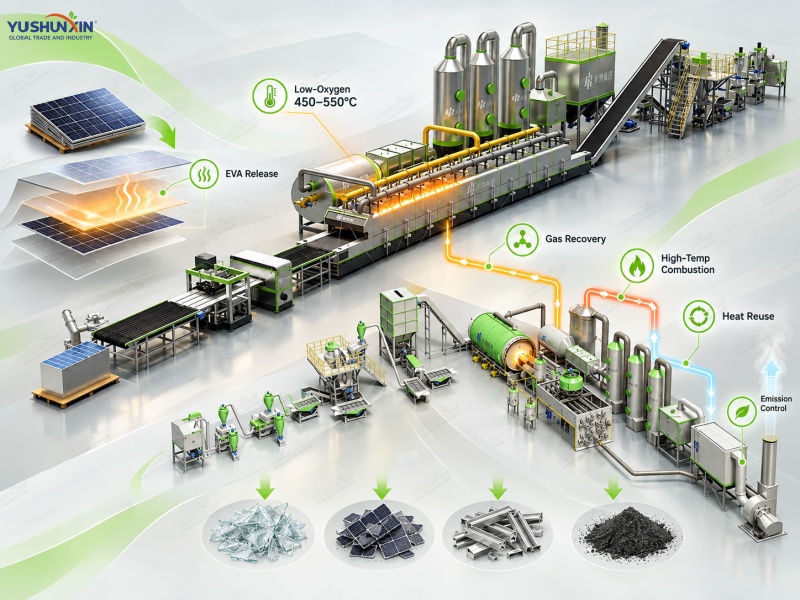
Thermal pyrolysis serves as the core technology for separating bonded photovoltaic layers. Rotary or tunnel pyrolysis furnaces maintain strict low-oxygen environments at 450 to 550 degrees Celsius. Por lo tanto, the system decomposes EVA encapsulants and polymer backsheets completely without damaging inner inorganic substrates. Además, captured pyrolysis gases undergo high-temperature combustion to provide supplemental thermal energy. De este modo, this energy-recycling mechanism significantly lowers operational heating costs while meeting rigorous environmental emission standards.
How Can Precious Metals and Silicon Materials Be Effectively Enriched?
03 · MaterialesHigh-value material extraction represents the primary profit driver for modern industrial recycling plants. Por lo tanto, our advanced hydrological and mechanical sorting systems effectively isolate cobre, plata, and high-purity silicon powders. Specialized physical separation machinery first extracts base metals like copper conductors and aluminum frames. Además, chemical leaching and electrowinning yield industrial-grade silver products with maximum market value. Mientras tanto, precision air separation and screening preserve recovered silicon fractions for downstream applications. Como consecuencia, plant operators unlock substantial revenue streams while establishing circular economy standards.
Physical Separation
and Multi-Metal Recovery
Multi-stage mechanical equipment efficiently separates base metals from cell residues without chemical pollution. For the pyrolysis method, after pyrolysis of photovoltaic panels, air separator and vibrating screener instantly isolate copper strips, large glass pieces and large silicon wafers. Además, two gravity separators remove small silicon wafers. And color sort can separate fine glass fibers and copper wires. For the mechanical method, gravity separator is used to separate copper form the mixture of silicon powder and the plastic particles. Después, electrostatic separators refine fine metal-plastic mixtures to achieve copper recovery rates above 95 percent. Por lo tanto, this physical processing route rapidly concentrates valuable copper and aluminum for direct industrial remelting.
Hydrometallurgical Silver Extraction
and Silicon Purification
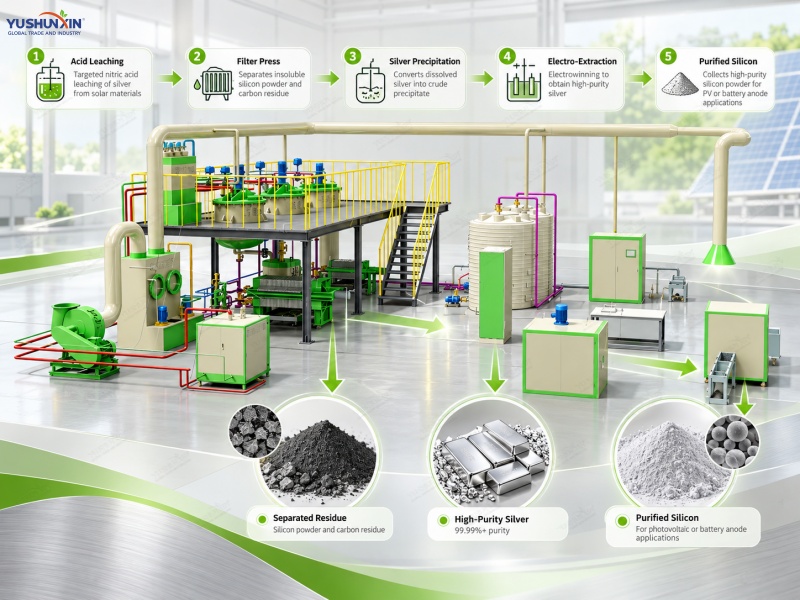
Hydrometallurgical processing offers superior recovery rates exceeding 98 percent for precious silver components. PPH acid-washing leaching reactors treat ground cell residues with targeted nitric acid solutions under precise temperature controls. Además, specialized filter presses isolate insoluble silicon powders and carbon residues from silver-bearing liquors. PPH displacement kettles then convert dissolved silver into crude precipitates using salt and iron agents. Además, electro-extraction cells refine silver solutions to yield certified bullion with purity exceeding 99.99 percent. Mientras tanto, secondary screening units collect purified silicon powders for photovoltaic or battery anode manufacturing. Como consecuencia, recyclers produce high-grade raw materials that command top market prices.
How Does the Off-Gas and Environmental Control Route Ensure Compliance?
04 · AmbienteIndustrial photovoltaic recycling plants must establish strictly compliant environmental controls for process off-gases. Thermal decomposition of EVA films and plastic backsheets generates complex hydrocarbons, acid fumes, and potential dioxin precursors. Por lo tanto, our integrated off-gas purification system employs multi-stage thermal and chemical treatments to neutralize hazardous emissions. Secondary high-temperature combustion first decomposes persistent organic pollutants at the source. Subsequently, rapid cooling and multi-stage scrubbing units eliminate acid vapors, particulates, and volatile organic compounds. Como consecuencia, plant operations fully satisfy international emissions regulations and preserve local environmental safety.
High-Temperature Thermal Cracking and Energy Recovery
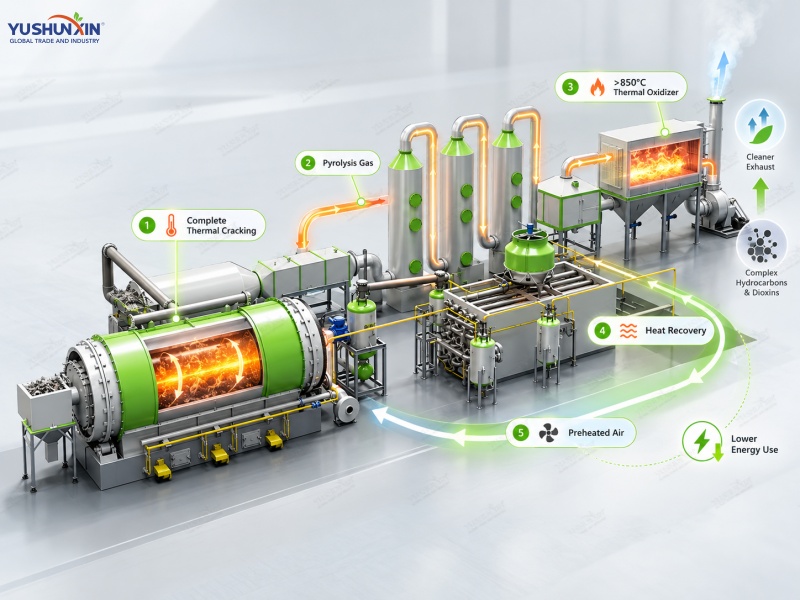
The primary thermal cracking phase eliminates toxic organic precursors through complete secondary combustion. Induced draft fans route volatile pyrolysis gases directly into a thermal oxidizer operating above 850°C. Under these extreme conditions, complex hydrocarbons and dioxin molecules rapidly break down into harmless carbon dioxide and water vapor. Además, a high-efficiency heat exchanger recovers high-temperature flue thermal energy to preheat intake air. This energy-recycled architecture significantly reduces plant electrical power requirements during steady-state operations. Por lo tanto, high-temperature thermal cracking solves potential toxic risks while lowering operational energy consumption.
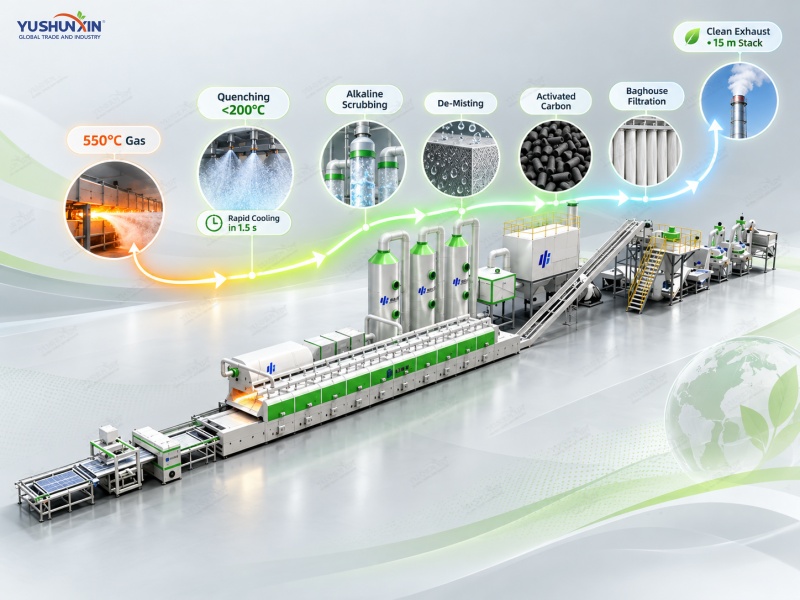
Rapid Cooling and Multi-Stage Flue Gas Purification
Preventing dioxin de novo synthesis requires precise thermal control during gas cooling. A dedicated quenching tower rapidly drops flue gas temperature from 550°C to below 200°C within 1.5 artículos de segunda clase. This extreme thermal drop effectively stops dioxins from reforming in downstream ductwork. Próximo, a wet alkaline scrubbing tower neutralizes fluorine and chlorine acid gases using caustic solutions. Following acid removal, de-misting units, activated carbon adsorption beds, and pulse jet baghouses strip remaining VOCs and ultra-fine dust particles. Como consecuencia, the purified exhaust exits through a 15-meter stack, completely fulfilling environmental standards.
What Is the Investment Cost and ROI Analysis for an Industrial Recycling Plant?
05 · InvestmentEstablishing a commercial photovoltaic recycling plant requires comprehensive financial planning for both CAPEX and OPEX. Primary capital expenditure focuses on core processing machinery, eco-friendly off-gas systems, and essential site infrastructure. Mientras tanto, operational expenditures incorporate raw panel acquisition, plant labor, utility power, and chemical reagents. Sin embargo, direct sales of high-purity recycled products generate robust daily cash flows. Además, higher processing capacities significantly optimize unit operating overhead. Como consecuencia, well-designed facilities achieve short payback periods and sustained profitability in the emerging market.
Comprehensive Capital Expenditure Infrastructure
Initial capital investments encompass processing equipment, wet silver refining lines, and factory infrastructure. Equipment expenditure for a standard 1-ton-per-hour pyrolysis line typically ranges between $555,556 y $694,444. Infrastructure construction requires a heavy-duty industrial shed spanning at least 3,000 square meters with reinforced concrete foundations. Plant owners must also allocate capital for power transformation units, wastewater neutralization reactors, and regional environmental permits. Por lo tanto, establishing a fully compliant recycling site demands balanced capital allocations across machinery and civil engineering.
Operating Expenditure and Production Cost Structure
Daily operating expenses primarily stem from raw material procurement, direct labor, and utility power. Purchasing single-glass modules averages $625 per ton, while double-glass modules cost around $486 per ton. Labor costs require approximately $174 daily for five operators managing automation lines. Operational power consumption accounts for $213 per day under optimized thermal-recycled setups. In wet silver extraction, chemical reagents like nitric acid and caustic soda add minor variable overheads. Como consecuencia, the total daily operating cost for processing 5 tons of single-glass modules reaches $3,512.
Recovered Material Commercialization and Revenue Generation
Selling multi-component recycled outputs yields high revenue margins per processed ton. Tratamiento 1 ton of single-glass modules generates 700 kg glass, 170 kg aluminum, 45 kg silicon, 15 kg copper, y 0.5 kg silver. Based on market prices, single-glass module outputs yield a total revenue of $1,095.06 per ton. High-purity silver and copper ribbons contribute over half of this core economic value. Mientras tanto, double-glass modules generate $830.72 per ton due to higher glass ratios. Por lo tanto, comprehensive material separation secures diverse market revenue streams.
How Can Modular Upgrades Scale Your E-Waste Recycling Business?
06 · BusinessIndustrial photovoltaic recycling plants must maintain long-term adaptability to capture emerging market opportunities. As global retirement volumes accelerate, facility operators frequently require flexible expansion strategies beyond standard glass and frame separation. Por lo tanto, our modular plant architecture enables seamless integration of advanced metallurgical refining and diversified e-waste processing units. Facility owners can incrementally introduce wet silver extraction modules to monetize precious metal recovery. Como consecuencia, scalable system upgrades transform basic recycling centers into comprehensive circular economy hubs.
Diversification into Broader E-Waste and Lithium Battery Streams
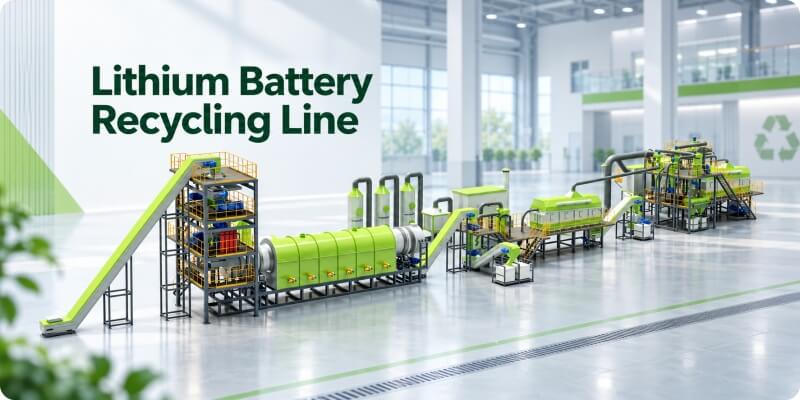
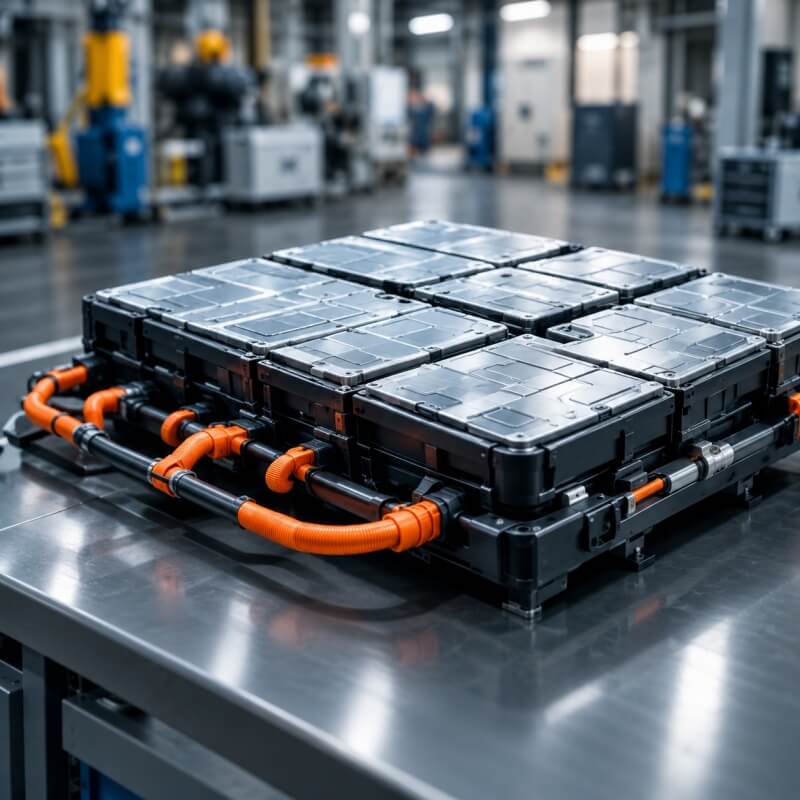
Commercial recycling hubs should diversify input materials to maintain high operational capacity year-round. The mechanical shredding and electrostatic separation units within our plant are natively compatible with waste lithium-ion batteries. Facility owners can adjust crushing blades and pneumatic classifiers to process diverse electronic waste streams. This multi-feedstock capability buffers seasonal fluctuations in photovoltaic panel retirements. Además, shared off-gas and dust removal infrastructure significantly reduces capital expenditures for secondary processing lines. Como consecuencia, material diversification safeguards business resilience and maximizes facility asset utilization.
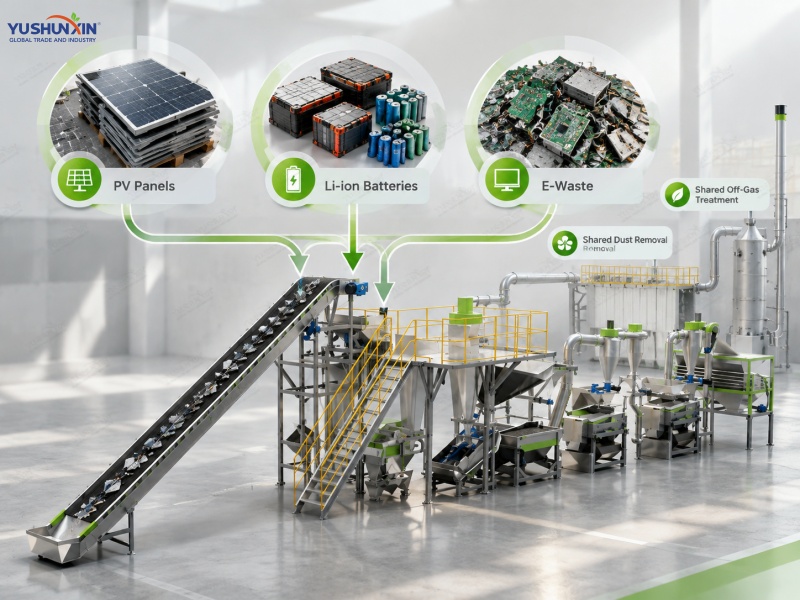
Incremental Integration of Precious Metal Refining
Maximizing financial returns relies heavily on secondary deep-processing modules for precious metals. While primary physical sorting recovers bulk glass and silicon, high-purity silver remains trapped in microscopic electrode residues. Plant operators can seamlessly couple chemical leaching and electrolytic refining units onto existing sorting lines. This secondary expansion processes fine silicon-silver powders into 99.99% pure silver ingots. Además, closed-loop wastewater treatment systems neutralize acidic byproducts and ensure absolute environmental compliance. Por lo tanto, incremental metallurgical integration unlocks high-margin revenue streams with minimal operational disruption.
Resumen
In summary, an advanced photovoltaic recycling plant combines efficient thermal pyrolysis, rigorous environmental controls, and automated physical sorting to achieve maximum resource recovery and high financial returns. By investing in modular systems, operators can seamlessly scale their processing capabilities, extract high-purity precious metals, and future-proof their operations in the growing circular economy. If you need other solar panel recycling solutions, como Línea de reciclaje de paneles solares de un solo vidrio., double-glass PV recycling plant y Línea de procesamiento de pirólisis de paneles solares., por favor contáctenos.
De tus necesidades
al impacto real


