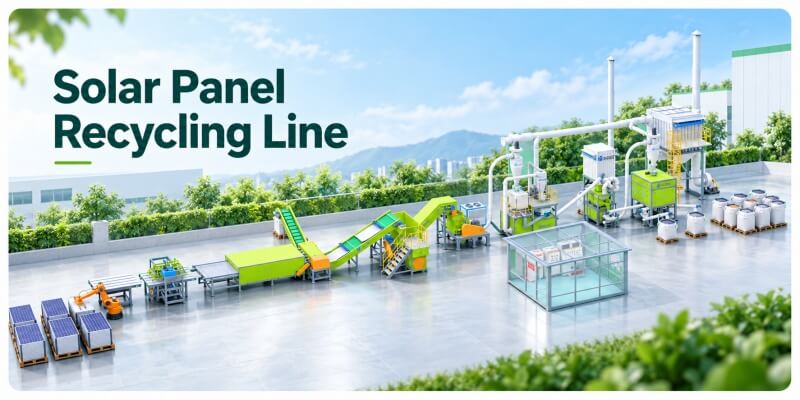
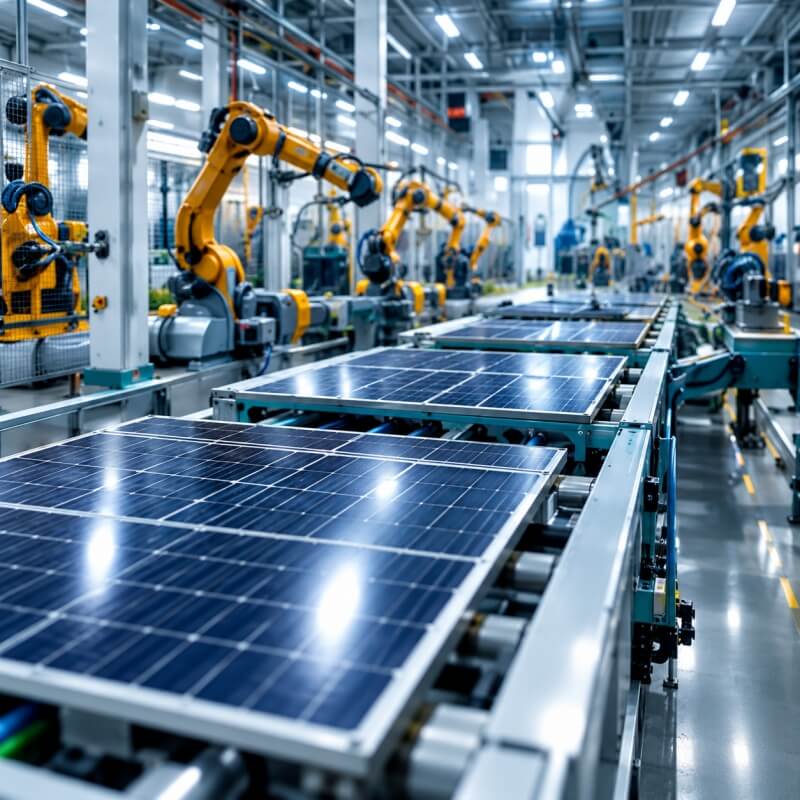
As solar panel production expands, factory scrap is becoming a measurable cost and recoverable resource. Rejected modules, broken cells, glass scrap, tabbing ribbons and laminated defects can no longer be treated as ordinary waste. For large PV manufacturers, an in-house recycling line can support material recovery, cleaner workshops, ESG reporting and compliant disposal. This article focuses on factory-side recycling planning. It covers mechanical separation, thermal delamination, material sorting and optional silver recovery.
How Should PV Factories Build A Scrap-To-Recovery System?
01 · SystemSolar panel factories produce stable scrap every day. Therefore, scrap recycling should follow a factory-side recovery plan. Rejected modules, broken cells, trimming waste and failed laminates can become recoverable material streams. Moreover, the system should reduce disposal cost and improve production waste control.
Map Scrap Sources Before Recycling
PV manufacturing scrap is cleaner and more stable than retired panels. Classifying defective modules, glass, aluminum, silicon, and copper scrap helps define the right recycling route.
Separate Materials For Higher Value
Factory recycling can recover glass, aluminum, copper, silicon, and silver-bearing materials separately. Clear material classification improves resource value, ESG tracking, and production waste management.
Match The Line With Scrap Flow
The recycling system should match scrap type, volume, and recovery targets. Mechanical separation suits clean scrap, while thermal routes support laminated materials and deeper material recovery.
How Does Each PV Scrap Type Match The Recycling Process?
02 · PV Scrap TypePV factories generate different scrap streams every day. Therefore, one recycling route cannot handle all materials well. Clean glass, laminated rejects, broken cells and metal parts need separate treatment. Since glass can account for about 70% of a standard PV module, early classification directly affects recovery value.
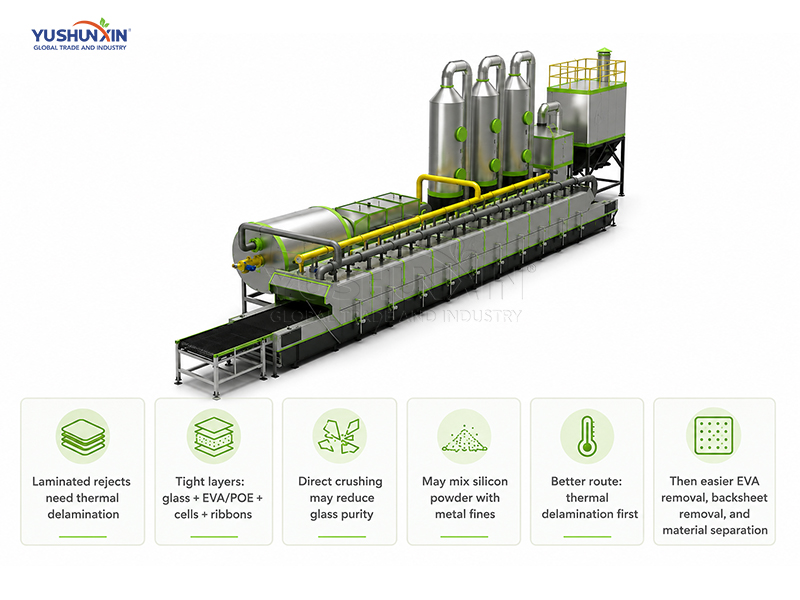
Laminated Rejects Need Thermal Delamination
Laminated rejects combine glass, EVA or POE, cells and ribbons tightly. Therefore, direct crushing may reduce glass purity. It can also mix silicon powder with metal fines. A better route uses thermal delamination first. Then, EVA removal, backsheet removal and material separation become easier.
Cell And Silicon Scrap Need Fine Sorting
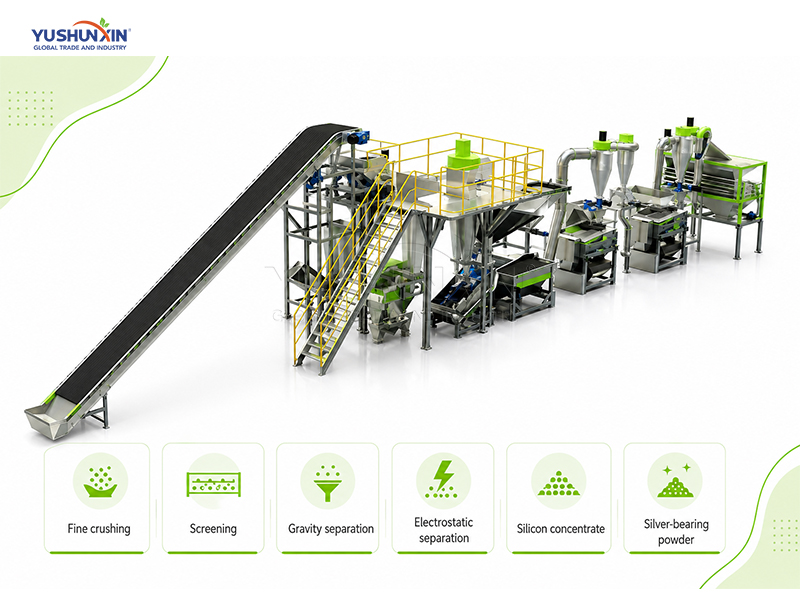
Broken cells, wafer scrap and silicon powder need precision separation. Therefore, heavy crushing is not the main step. The route should include fine crushing, screening, gravity separation and electrostatic separation. Moreover, this process can concentrate silicon and silver-bearing powder.
Metal Parts Need Early Removal
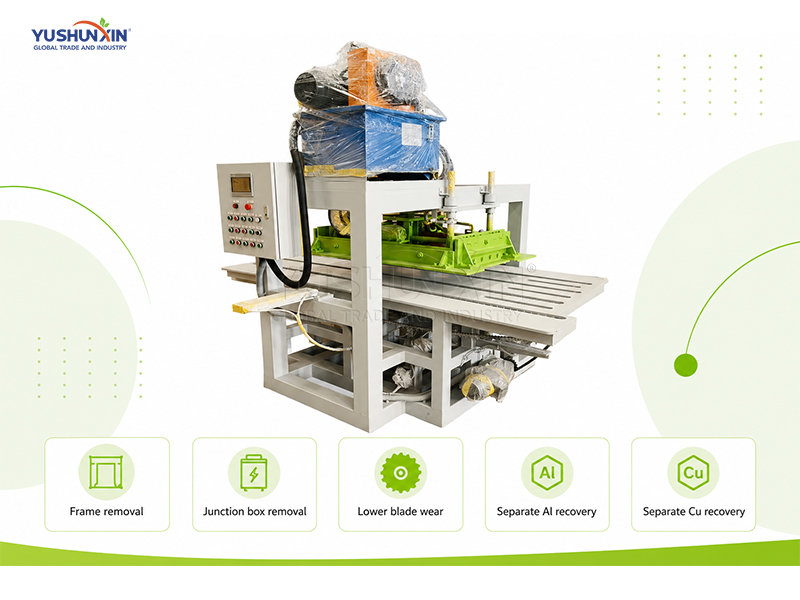
Aluminum frames, junction boxes and copper ribbons should leave before deep processing. Otherwise, they increase blade wear and sorting pressure. The front-end route should include frame removal and junction box removal. Then, aluminum and copper can enter separate recovery channels.
How Can PV Scrap Recycling Fit Factory Production Flow?
03 · Production Flow
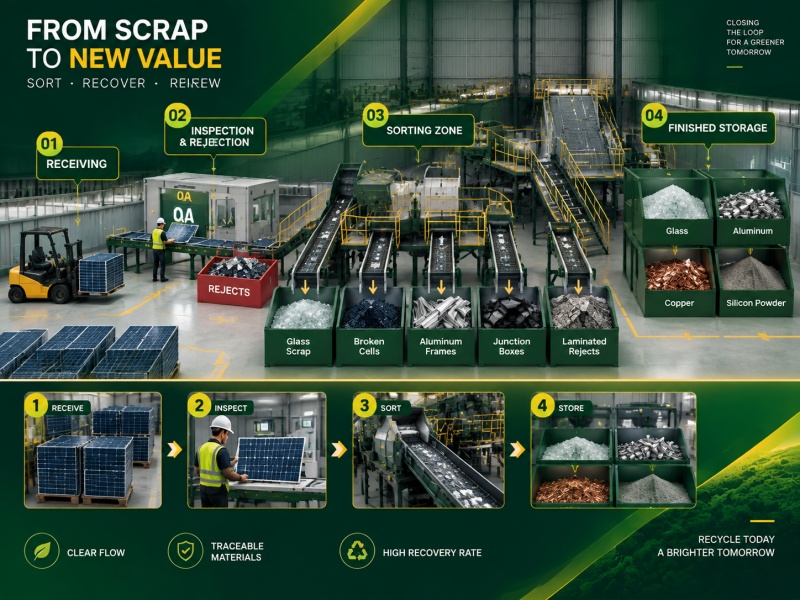
PV factories need a recycling line that follows daily production flow. Scrap usually comes from lamination, trimming, framing, testing and quality rejection. Therefore, the layout should include scrap buffering, sorting, recycling and finished material storage. This arrangement reduces handling distance, keeps workshops cleaner and avoids production interruption.
Scrap Receiving Near
Rejection Points
The scrap buffer zone should stay close to inspection and rejection areas. Then, workers can move defective panels quickly. Next, the sorting zone separates glass scrap, broken cells, aluminum frames, junction boxes and laminated rejects. This step helps each material enter the right recovery route. Finally, recovered glass, aluminum, copper and silicon powder should move to finished storage. This keeps material flow clear and traceable.
Mechanical Line For Clean
Single-Glass Scrap
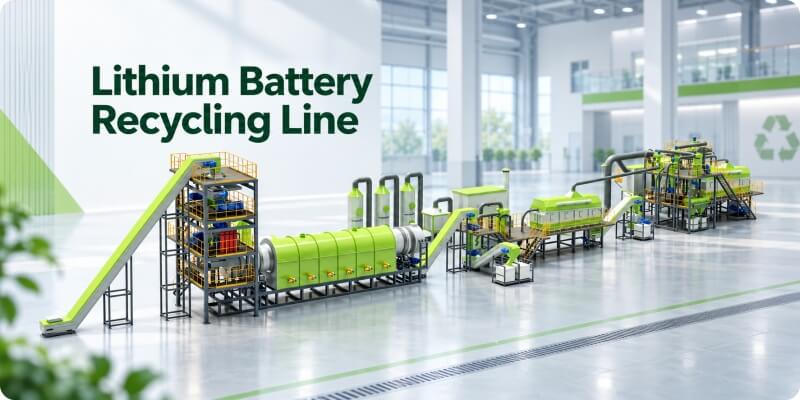
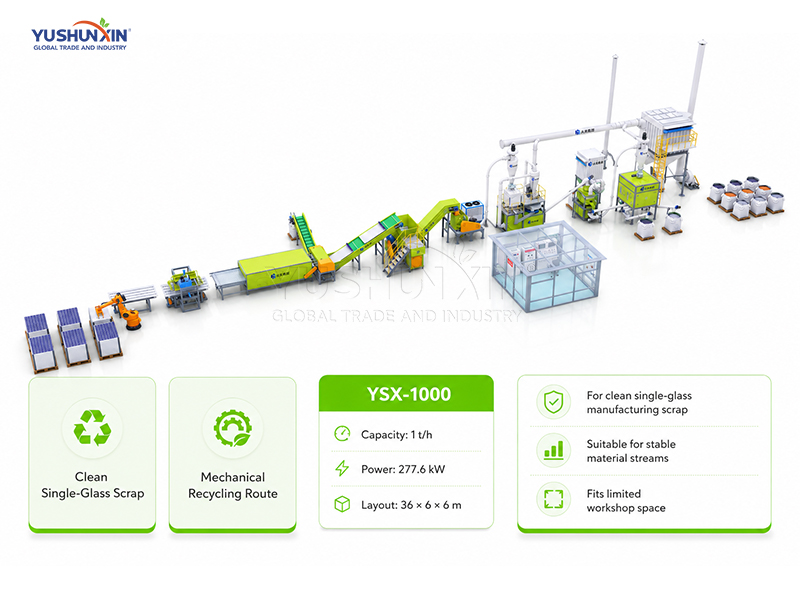
For clean single-glass manufacturing scrap, YSX-1000 is a suitable mechanical recycling option. It supports 1 t/h capacity, with 277.6 kW power and about 36×6×6 m layout space. This line suits factories with stable single-glass scrap, cleaner material streams and limited workshop space.
Pyrolysis Line For
Mixed Laminated Scrap
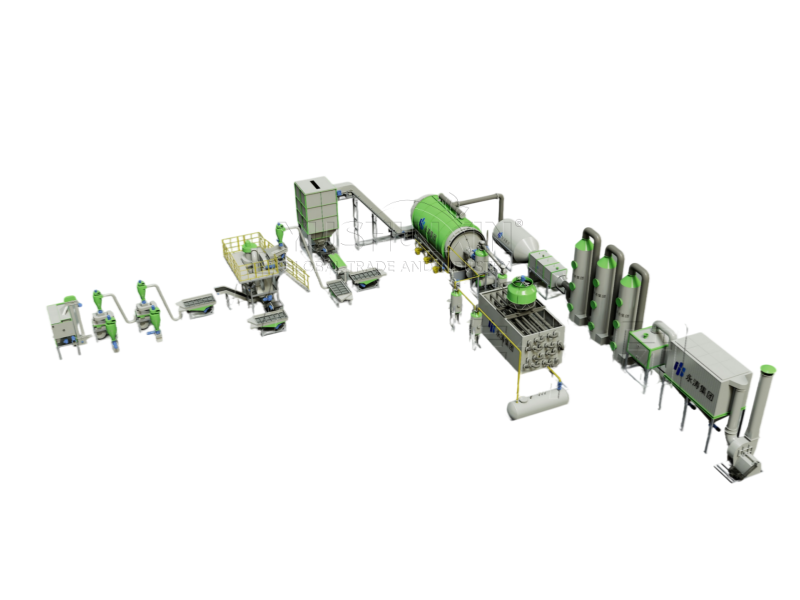
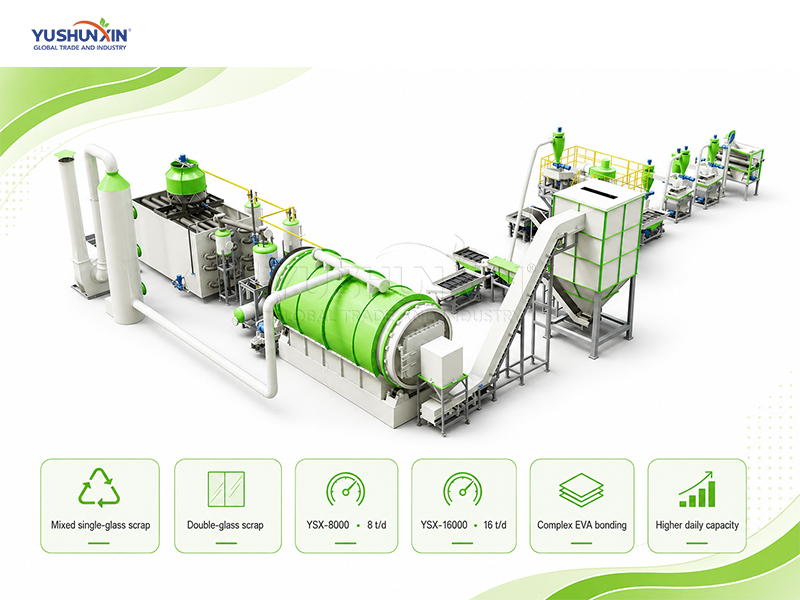
For mixed single-glass and double-glass laminated scrap, YSX-8000 and YSX-16000 are better options. YSX-8000 supports 8 t/d, while YSX-16000 supports 16 t/d. These lines suit factories with multi-type scrap, complex EVA bonding and higher daily processing demand.
How Does Pyrolysis Method Improve Factory Scrap Separation?
04 · Pyrolysis Method
PV factory scrap often includes laminated rejects. Therefore, factories need more than direct crushing before sorting. Thermal delamination gives solar panel factories a controlled separation route. It weakens EVA or POE bonding under low-oxygen heat. Then, glass, silicon, tabbing ribbons and fine powder can enter cleaner downstream sorting.
Low-Oxygen Pyrolysis Separates Materials Before Fine Sorting
Pyrolysis does not burn factory scrap as waste. Instead, the system uses low-oxygen pyrolysis to remove EVA and POE bonding. Meanwhile, the laminated structure gradually loses adhesion during controlled heating. Then, glass pieces separate more easily from silicon cells and metal ribbons. Therefore, the sorting system can reduce mixed material contamination. For factories, this means better glass recovery and cleaner silicon-rich material. It also reduces the pressure on vibrating screens, air separators and electrostatic separators.
Heat Recovery Lowers Operating Pressure
Pyrolysis method also creates combustible pyrolysis gas. Therefore, the system can send gas back to the burner. This gas reuse helps reduce external fuel demand. Meanwhile, electric heating can support startup and low-load operation. So, the furnace keeps a stable temperature during different factory shifts. However, gas reuse must work with emission control. A complete line should include flue gas treatment, dust collection and gas cleaning. For example, the system can use quenching, alkaline spraying and activated carbon adsorption. Then, pulse bag dust collection can control fine particles before discharge. This solution helps factories combine recovery value, cleaner production and compliance review.
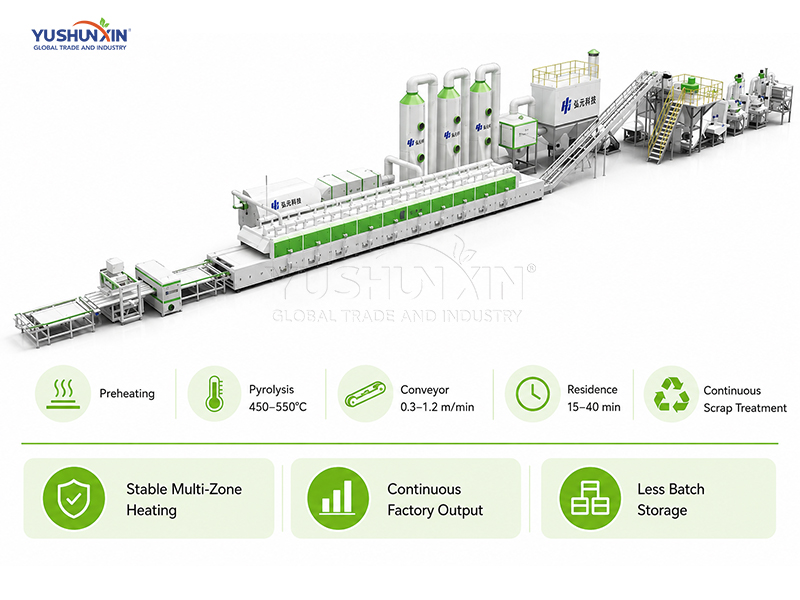
Continuous Tunnel Furnace Stabilizes Factory Scrap Treatment
A continuous tunnel furnace suits factories with daily scrap output. The furnace can use several temperature zones for stable treatment. For example, the process may include preheating, main pyrolysis and cooling zones. The main pyrolysis zone usually runs around 450–550℃ for EVA carbonization. Meanwhile, the conveyor speed can match scrap volume and residence time. Some designs use 0.3–1.2 m/min conveyor speed. This can support about 15–40 minutes of thermal residence time. Therefore, the factory can process scrap continuously. It also avoids unstable batch handling and scattered workshop storage.
Get your Solution!How Can Recovered Materials Support Factory Payback?
05 · MaterialsSolar panel factories should focus on materials with clear resale value. Therefore, the recycling solution should separate bulk glass, high-value silicon powder, silver-bearing fractions, copper and aluminum.
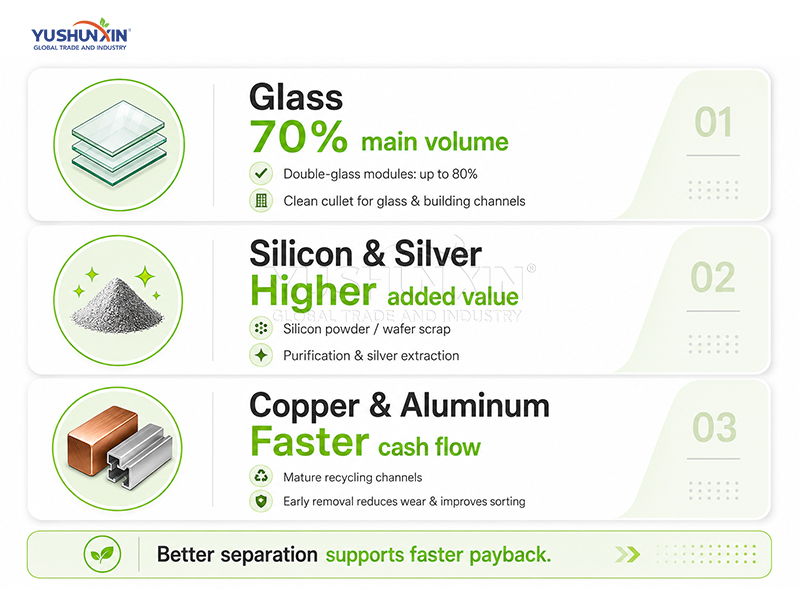
Glass Builds The Main Recovery Volume
Glass is the largest recovered material. In common modules, glass can account for about 70%. Moreover, double-glass modules may reach about 80%. Therefore, clean glass separation matters. High-purity glass cullet can enter glass factories, building material plants or reprocessing channels.
Silicon And Silver Fractions Increase Added Value
Silicon wafers, silicon powder and silver-bearing powder support higher-value recovery. However, they should enter further purification, silver extraction or metallurgical recovery. Therefore, fine crushing, screening and separation should improve material concentration first.
Copper And Aluminum Improve Cash Flow
How Can A PV Scrap Recycling Project Pass Technical And Financial Review?
06 · Review
Industrial PV factories need a reviewable project package before purchase. Therefore, the solution should show compliance, safety, layout and ROI together. Procurement teams need more than machine photos. They need documents, process logic and measurable recovery value for internal approval.
Compliance Package Defines Project Readiness
A complete PV scrap recycling solution should include CE documents, electrical safety design and mechanical safety details. Also, the supplier should provide a process flowchart, layout drawing, equipment list and emission control plan. These documents help EHS, production and finance teams review the project together. For European, Middle Eastern and Southeast Asian factories, this package can reduce approval uncertainty.
Integrated Safety System Controls Gas, Dust And Heat
PV laminated scrap may involve EVA, POE, backsheet material and fine dust. Therefore, the recycling line should control oxygen, temperature, pressure and exhaust gas. A pyrolysis recycling system can use low-oxygen operation and slight negative pressure. Meanwhile, oxygen monitoring and temperature monitoring help stabilize the furnace process. For exhaust treatment, the line can use quenching, alkali spraying, condensation, activated carbon and pulse dust collection.
ROI Model Links Disposal Savings With Material Recovery
A strong ROI model should not only calculate silver recovery. Instead, it should combine waste handling savings and recovered material value. Standard PV modules may contain about 70% glass. Moreover, double-glass modules may contain about 80% glass. So, recovered glass, aluminum, copper, silicon and silver-bearing powder all affect payback. Labor reduction, cleaner workshops and ESG reporting also support long-term factory value.
Summary
We can provide a complete PV manufacturing scrap recycling solution for solar panel factories. Our solution starts from scrap classification and factory layout planning. Then, we match mechanical separation, pyrolysis method, fine sorting, emission treatment and optional silver recovery. For clean single-glass scrap, we can provide a mechanical solar panel recycling line. For mixed laminated modules, we can design a PV module pyrolysis recycling line for better delamination and material separation. Also, we can support equipment configuration, process flow design, layout drawings, compliance documents and ROI evaluation. Therefore, your factory can turn production scrap into recoverable glass, aluminum, copper, silicon and silver-bearing materials.
From Your Needs
to Real Impact


