As EV fleets enter large-scale retirement, automotive recycling networks need stronger battery handling capacity. End-of-life EV battery waste management now affects compliance, safety and profit. For dismantlers, collection hubs and recycling investors, the key is a reliable recovery route. That route should connect battery sorting, увольнять, демонтаж, сокрушительный, separation and black mass recovery. The focus should be clear: более безопасная работа, higher material value and equipment planning for industrial recycling projects.
How Do EV Battery Networks Route Mixed Battery Sources Into Centralized Recovery?
01 · MixedAutomotive recycling networks will face mixed battery flows from ELVs, accident vehicles, service centers, insurers and fleet renewal projects. IEA data shows battery recycling capacity reached 300 GWh in 2023, and announced projects may exceed 1,500 GWh by 2030. EV battery retirement will then grow faster after the mid-2030s. Так, the first task is not equipment purchase. It is source mapping, regional collection and centralized recovery planning.
Map Battery Sources Before Capacity Planning
Battery sources such as EVs, buses, fleets, and repair centers have different conditions. Source mapping helps define storage, увольнять, транспорт, and processing requirements.
Build Regional Hubs For Collection
Regional hubs can handle weighing, registration, сортировка, and safety checks before transportation. This reduces logistics risk and provides cleaner battery data for the recycling plant.
Centralize Recovery To Improve Efficiency
Not every dismantling site needs a full recycling line. Centralized recovery combines discharge, демонтаж, сокрушительный, разделение, and dust control to improve equipment utilization and black mass quality.
How Can Battery Grading Create A Safer EV Battery Recycling Solution?
02 · Battery GradingAs EV battery inflow grows, recyclers cannot use one route for every pack. Battery condition should decide the next step first. Then the project can reduce fire risk, protect equipment, and improve material value.
Reusable Batteries Need Second-Life Evaluation
Batteries with remaining value should enter testing, оценивание, and second-life assessment first. This route helps maximize battery value before material recovery.
Scrap Batteries Need Material Recovery
Batteries without reuse value should enter discharge, демонтаж, сокрушительный, и разделение. The goal is to recover black mass, медь, алюминий, сталь, и пластик.
High-Risk Batteries Need Safe Pretreatment
Damaged batteries require isolation, инспекция, and controlled handling before processing. Safety systems such as fire protection, очистка газа, and dust control reduce operational risks.
How to Configure The Recycling Line For Automotive Battery Networks?
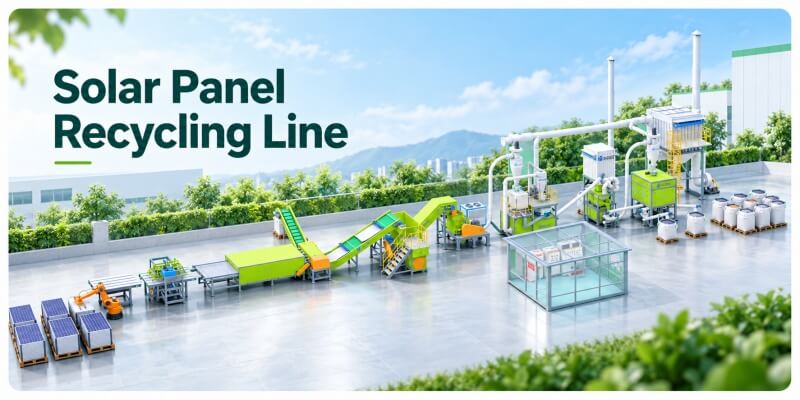
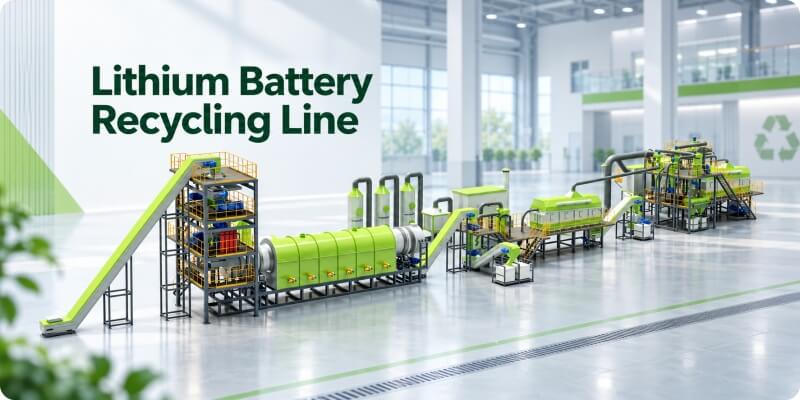
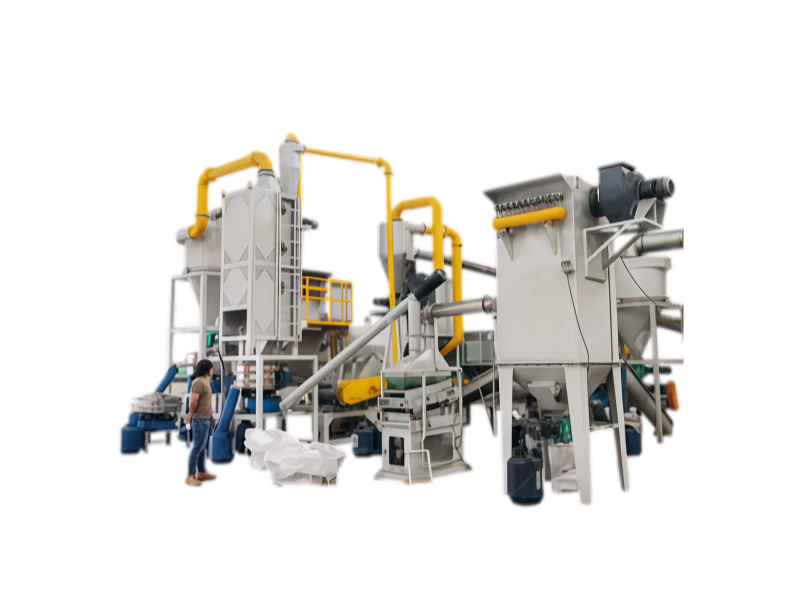
03 · КонфигурацияAutomotive recycling networks need a system, not only one machine. A practical EV battery recycling line should match battery packs, модули и ячейки. It should also support safe discharge, controlled dismantling, stable crushing, черная месса recovery and compliant dust control. Для промышленных проектов, the line can start from 500 кг/ч или 1,000 кг/ч, then expand with higher feedstock volume.
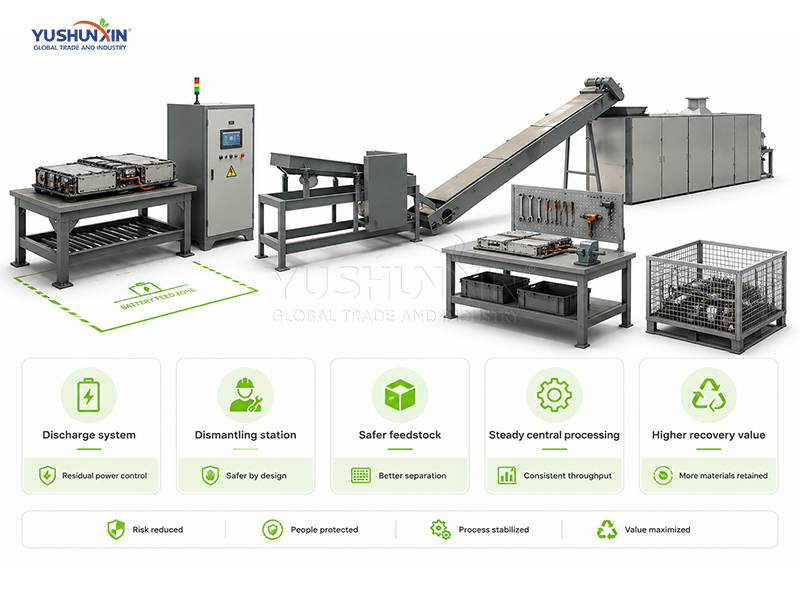
Discharge and dismantling
reduce front-end risk
The first step should control residual power. А discharge system helps lower electrical risk before cutting or dismantling. Затем, manual or semi-automatic dismantling stations handle battery packs and modules. Operators can remove shells, wiring harnesses, BMS parts and large metal frames. This process reduces the load on the crusher. It also improves downstream separation accuracy. For automotive recycling networks, this stage works well near dismantling hubs. It turns mixed EV battery waste into safer feedstock. Затем, the central plant can process materials more steadily.
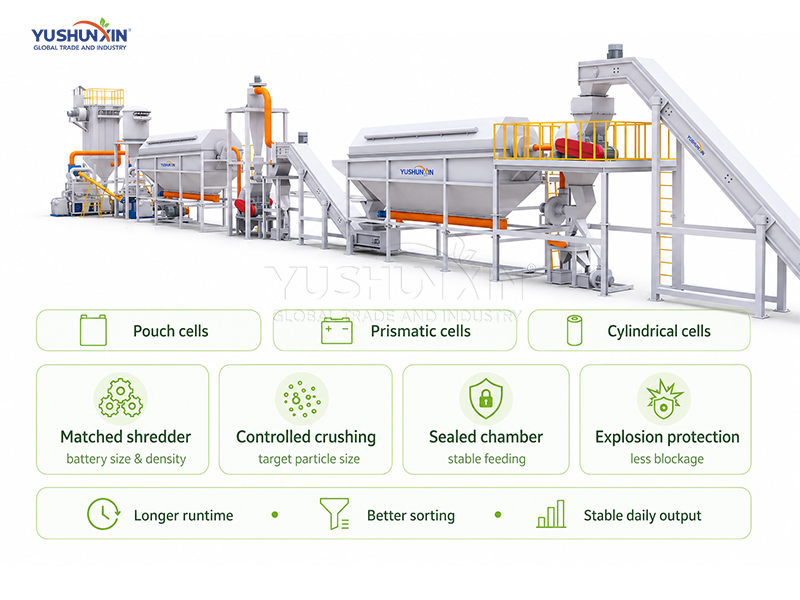
Shredding and crushing
should follow battery structure
Different batteries need different crushing logic. Soft pouch cells, prismatic cells and cylindrical cells behave differently. Mixed modules also create higher requirements for feeding and sealing. Поэтому, the shredder should match battery size and packing density. The crusher should match target particle size and downstream sorting needs. Нож носить, chamber sealing and explosion protection also matter. For large networks, stable feeding matters more than peak capacity. A line with matched shredding and crushing reduces blockage. It also improves daily running time.
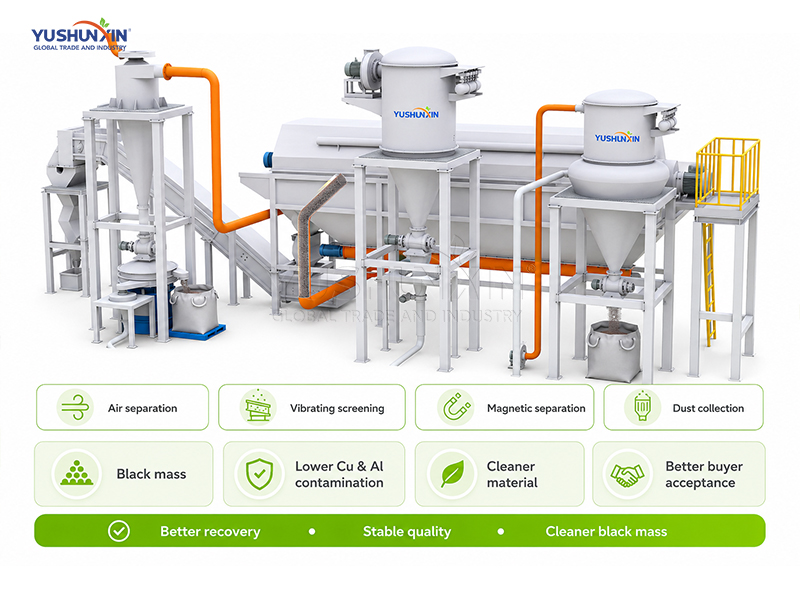
Air separation and screening
improve black mass recovery
После дробления, the line should separate valuable fractions quickly. Air separation removes light plastic, film and separator material. Vibrating screening classifies powder and granules by size. Magnetic separation removes iron and steel parts. Затем, copper and aluminum can enter further separation. Dust collection keeps fine black mass under better control. This configuration helps improve black mass quality. It also reduces copper and aluminum contamination. Как результат, downstream buyers receive cleaner material.
Environmental control
supports project approval
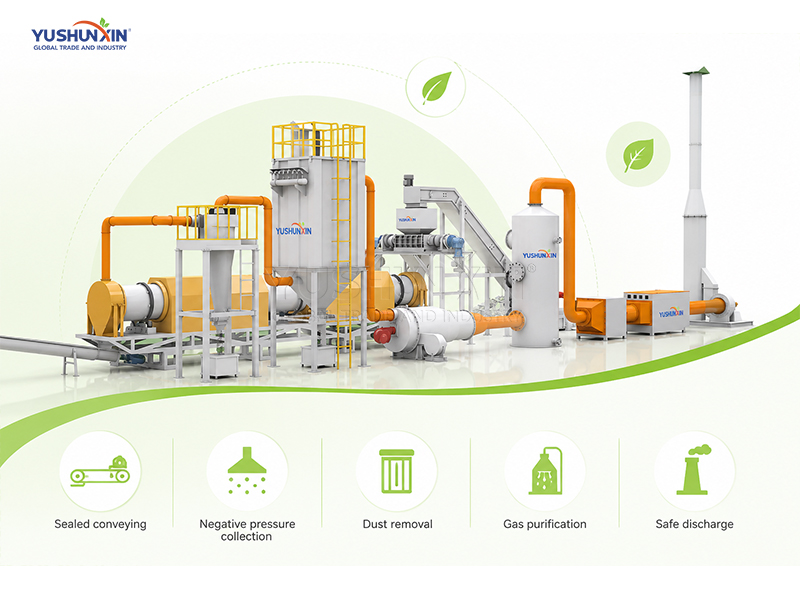
EV battery recycling creates dust and exhaust risk. Так, the line needs sealed conveying and negative pressure collection. It also needs dust removal, gas purification and safe discharge points. Spray towers, filters and collection systems can match local rules. The exact design depends on feedstock and approval standards. For automotive recycling groups, this part supports permits and audits. High-value customers should not only compare machine price. They should request layout drawings, process flow, safety design and emission plans. These documents help the project move from quotation to approval.
How Should Recovery Products Build A Stronger Revenue Model?
04 · Recovery ProductsAutomotive recycling networks should not rely only on steel and vehicle parts. EV batteries add a new material profit layer. A complete линия по переработке литиевых батарей может восстановить черную массу, медь, aluminum and steel. Поэтому, the project should plan product value before equipment selection. This helps investors judge output quality, cash flow and downstream sales channels.
Black Mass Should Define The Main Recovery Direction
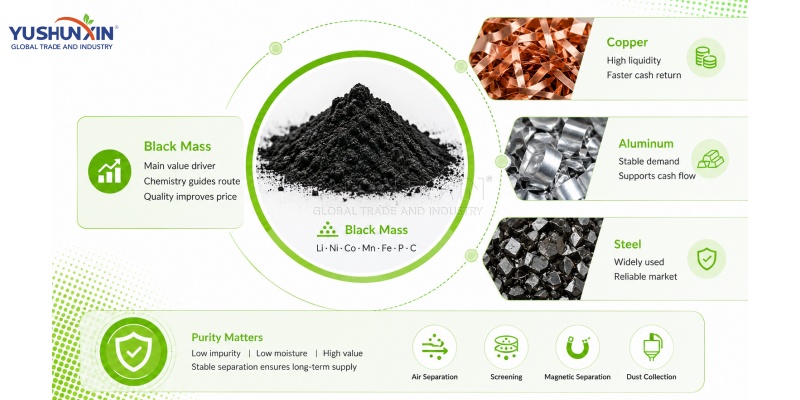
Black mass comes from cathode and anode materials. It may contain lithium, никель, кобальт, марганец, железо, phosphorus and graphite. In NMC battery projects, nickel and cobalt usually drive higher material value. In LFP battery projects, lithium recovery and large processing volume matter more. Поэтому, the battery chemistry should guide the recycling route. For automotive recycling networks, black mass quality directly affects project return. A stable crushing and separation system can reduce metal impurities. Затем, the material becomes easier to sell to hydrometallurgy plants.
Copper And Aluminum Should Support Faster Cash Return
Battery recycling profit should not wait only for black mass sales. Copper foil, aluminum foil, aluminum shells and steel casings can create quicker cash flow. Copper often has stronger market liquidity. Aluminum also has stable demand in metal recycling channels. Поэтому, these by-products can reduce pressure during early operation. A well-designed line should separate metals before they contaminate black mass. This improves both product value and daily settlement efficiency.
Product Purity Should Match Downstream Buyer Standards
Downstream buyers care about purity, moisture and impurity control. Медь, алюминий, пластмассы, separators and dust can lower black mass price. Поэтому, equipment configuration must support stable separation. Разделение воздушного потока, скрининг, magnetic separation and dust collection should work together. If product quality stays consistent, recycling networks gain stronger bargaining power. They can also build long-term supply relationships with refiners and battery material companies.
Получите свое решение!How Can A Safety Approval Package Support EV Battery Recycling Networks?
05 · Approval PackageEV battery recycling projects carry fire, dust and compliance risks. Поэтому, investors need a safety approval package before equipment purchase. The package should connect battery receiving, увольнять, демонтаж, сокрушительный, separation and emission treatment. It also helps automotive recycling networks pass factory review, insurer review and environmental approval.
SCREENING
Battery Risk Screening Should Start At The Receiving Area
Safety control starts when batteries enter the site. Operators should record battery type, Напряжение, масса, appearance and source. Затем, the site should test SOC before storage or dismantling. Batteries with leakage, swelling, deformation or abnormal heat need separate isolation. A high-risk battery zone should use clear spacing, fire partitions and temperature monitoring. This reduces fire spread before crushing begins. For automotive recycling networks, this step protects the whole plant. It also helps create traceable records for each battery batch.
AND AIR CONTROL
Enclosed Crushing And Air Control Reduce Operating Risk
Battery crushing and screening can release fine dust, electrolyte odor and organic gas. So the line needs enclosed conveying and negative-pressure collection. Dust should enter a dedicated filtration system. Gas should enter purification equipment before discharge. The plant should also match explosion-proof design, emergency stop points and online temperature monitoring. These details support stable industrial operation. For high-capacity projects, the safety design should follow the whole process. It should not only protect the crusher.
DOCUMENTS
Project Documents Should Match Approval And Audit Needs
Large clients usually need more than equipment pictures. They need a complete project document package. This package should include process flow diagrams, plant layout drawings and electrical control descriptions. It should also include safety plans and emission treatment plans. For European, Middle Eastern and industrial clients, CE documents or related certificates add trust. They also support customs clearance and project approval. A clear document package shortens communication time. It also helps buyers compare suppliers with real engineering standards.
How Can A Phased EV Battery Recycling Plan Protect ROI?
06 · Окупаемость инвестиций
For automotive recycling networks, EV battery recycling is an asset upgrade. ROI should not start with equipment price alone. It should start with battery supply, мощность обработки, качество продукции, labor cost and buyer channels. A stronger plan connects the first production line with future expansion. This helps investors control early risk and prepare for larger battery volumes.
Match Capacity With Battery Supply
Line capacity should match secured battery volume. Ежемесячная поставка, pack weight, and battery type help customers select suitable processing capacity.
Choose Automation By Project Needs
Automation level affects labor cost and operation stability. Small projects may use flexible operation, while large centers need automated feeding, сокрушительный, скрининг, и контроль пыли.
Define Product Routes Before Investment
Project value depends on clear product outlets. Черная месса, медь, алюминий, and other materials need reliable downstream buyers before final equipment configuration.
Зарезервируйте место для будущего расширения
A modular layout supports phased investment. Initial lines can expand with additional processing and environmental modules as battery supply grows.
Краткое содержание
End-of-life EV battery waste management now requires a planned industrial solution, not simple battery storage. Automotive recycling networks need to connect collection, инспекция, увольнять, демонтаж, сокрушительный, разделение, black mass recovery and environmental control. Юшуньсинь can provide a complete EV battery recycling solution based on your battery source, capacity target, требования безопасности, plant layout and product sales plan. Our team can help you configure suitable equipment, plan phased expansion and build a practical route for long-term recycling value.
Из ваших потребностей
к реальному воздействию


