As large-scale energy storage projects enter replacement cycles, retired LFP batteries are becoming a planned asset-management issue. Operators now need a safer route for collection, увольнять, демонтаж, crushing and material recovery. This article focuses on how ESS owners can build a controlled disposal plan, reduce site risk, meet compliance needs and match the right LFP battery recycling equipment with future recovery value.
How Can ESS Operators Convert Battery Retirement Pressure Into A Disposal Plan?
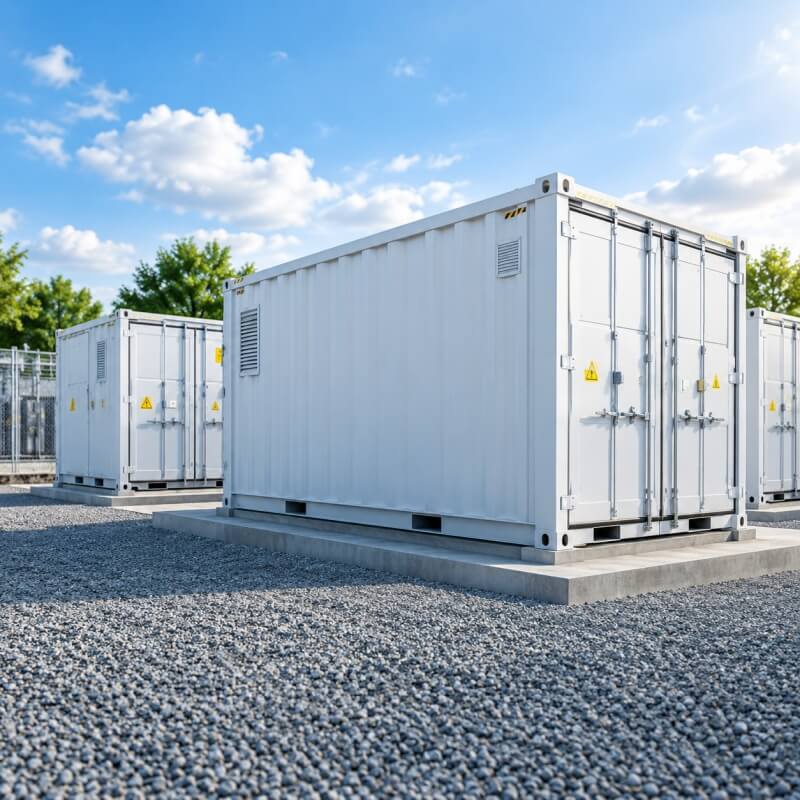
01 · Disposal PlanLarge ESS projects create battery retirement in concentrated batches. IEA data shows the global battery storage market doubled in 2023. It reached over 90 GWh that year. Поэтому, future LFP battery disposal will move from small recycling orders to planned industrial projects. Energy storage operators need a route before replacement starts. This route should cover sorting, тестирование, увольнять, открытие упаковки, crushing and material separation. Затем, each retired battery batch can leave the site with lower risk and clearer responsibility.
Centralized ESS Retirement Creates Storage Pressure
Retired ESS batteries often arrive as cabinets, пакеты, or modules, creating rapid storage pressure. Sorting, тестирование, увольнять, демонтаж, and crushing areas help prevent mixed handling and transfer delays.
Early Disposal Planning Reduces Project Risk
Disposal planning should start before battery replacement. Early preparation supports safe transport, clear disposal records, shorter shutdown periods, and stable recovery of black mass and valuable metals.
How Can Operators Build An Entry-Control Route Before Recycling?
02 · Entry-Control RouteLFP now dominates utility-scale storage. IEA says it covered over 90% of global BESS in 2025. So retired LFP battery disposal needs an entry-control route, not random receiving. Operators should classify batteries before the line starts. This step protects discharge, демонтаж, crushing and separation equipment.
Project-Based Receiving Creates The First Safety Gate
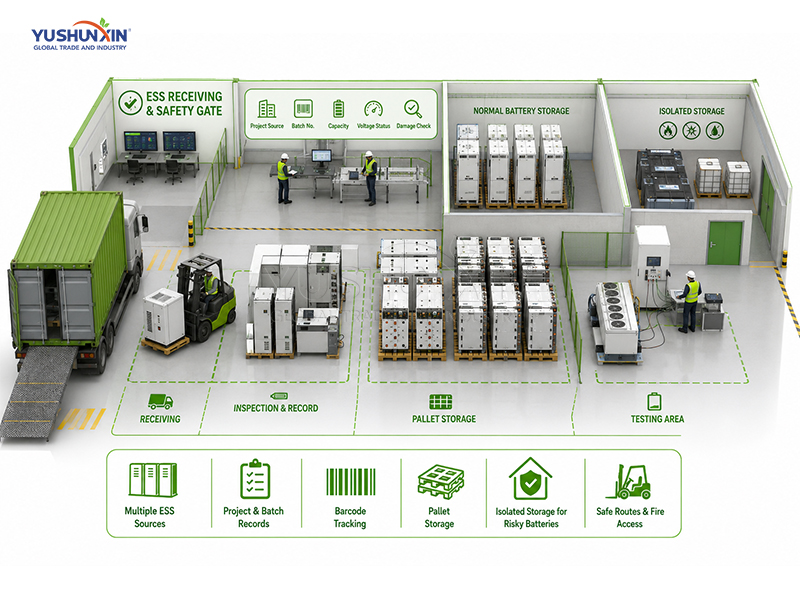
Retired ESS batteries may arrive as cabinets, стеллажи, пакеты, модули или ячейки. Поэтому, each source needs a different receiving method. Operators should record the project source, batch number, емкость, voltage status and visible damage. Затем, the plant can separate normal batteries from risky batteries. For large ESS projects, barcode tracking helps control every batch. Pallet storage also keeps batteries stable before testing. Тем временем, an isolated storage room keeps swollen, burned or leaking batteries away from the main line. The receiving area should include clear forklift routes and fire access. This layout reduces handling mistakes before battery recycling equipment starts.
Pre-Inspection Defines The Next Treatment Path
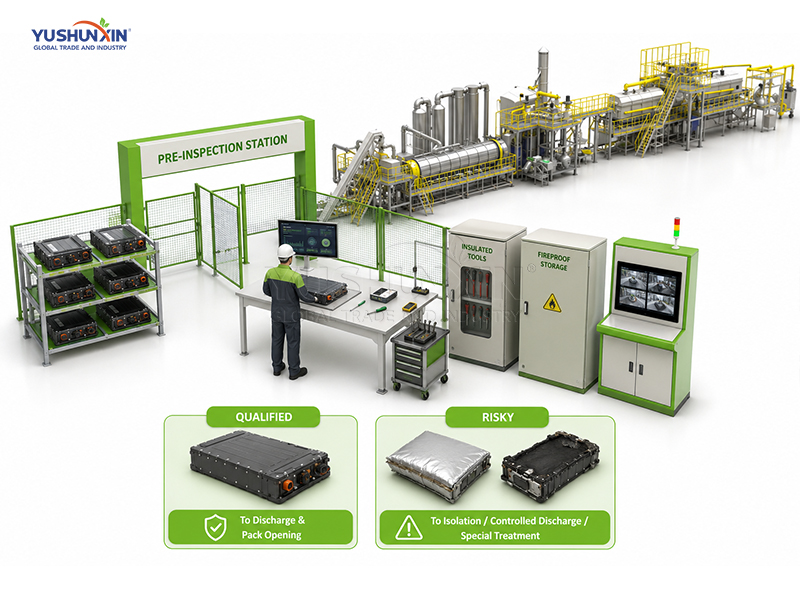
Pre-inspection should work as a line-entry rule. It should not work as a simple visual check. Operators need to check voltage, surface temperature, shell deformation and leakage. If one battery shows damage, it should not enter the main dismantling line. Затем, the team can choose the right route. Qualified batteries move to discharge and pack opening. Risky batteries move to isolation, controlled discharge or special treatment. This section can connect with a testing table, insulated tools, fireproof temporary storage and monitoring systems. These units help the recycling line run with fewer shutdowns.
How Can A Zoned ESS Battery Recycling Layout Handle Batch Retirement?
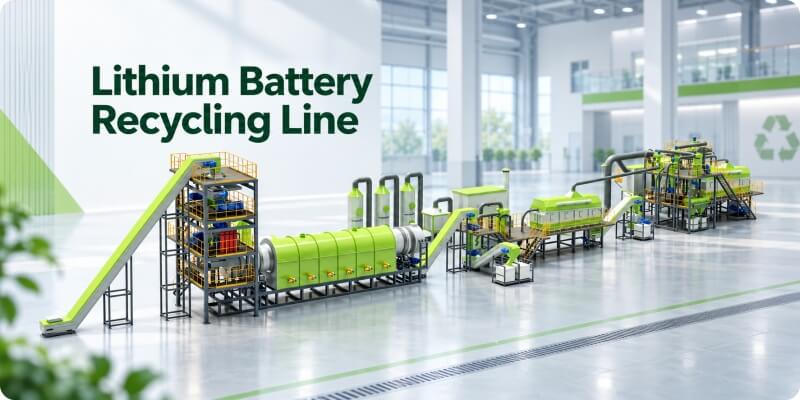
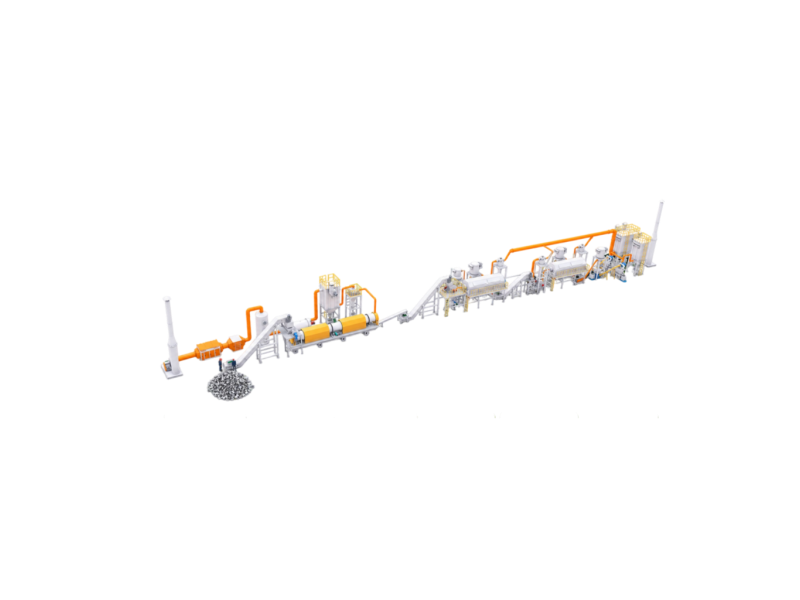
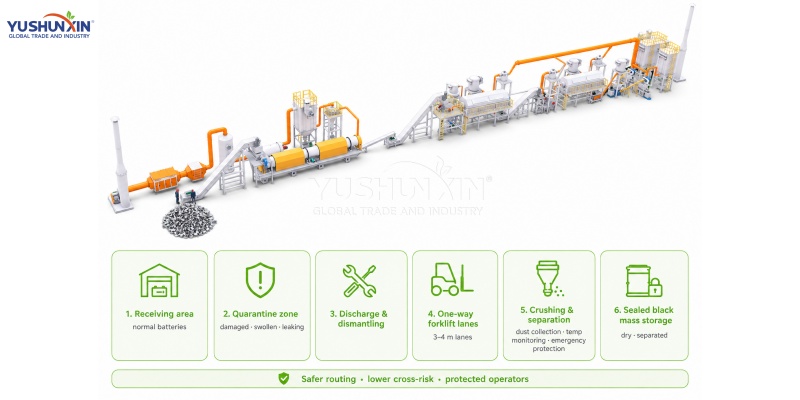
03 · LayoutUtility-scale ESS operators need more than one recycling machine. They need a layout that can receive battery cabinets, modules and packs in batches. Поэтому, the plant should divide risk, traffic and processing steps from the start. Практичный ESS battery recycling plant layout should connect receiving, карантин, тестирование, увольнять, демонтаж, сокрушительный, separation and black mass storage.
Controlled Processing Reduces Cross-Risk
Crushing and separation areas should connect with dust collection, мониторинг температуры, and emergency protection. Sealed black mass storage keeps recovered materials safer and cleaner.
Expansion Space Supports Future Capacity
The first layout should reserve space for future equipment and utilities. This allows phased capacity expansion while reducing reconstruction costs and supporting long-term ESS recycling.
Risk Zones Protect Battery Handling
Normal and damaged batteries should be stored separately. Quarantine, инспекция, and discharge zones help control fire and handling risks before dismantling.
Получите свое решение!What Equipment Solution Can Secure Retired LFP Battery Processing?
04 · EquipmentLFP chemistry offers better thermal stability than some battery types. Однако, retired ESS batteries still carry electrical and mechanical risk. Поэтому, the equipment route should control voltage first. Then it should manage heat, dust and abnormal batteries. This solution helps operators protect people, materials and production continuity.
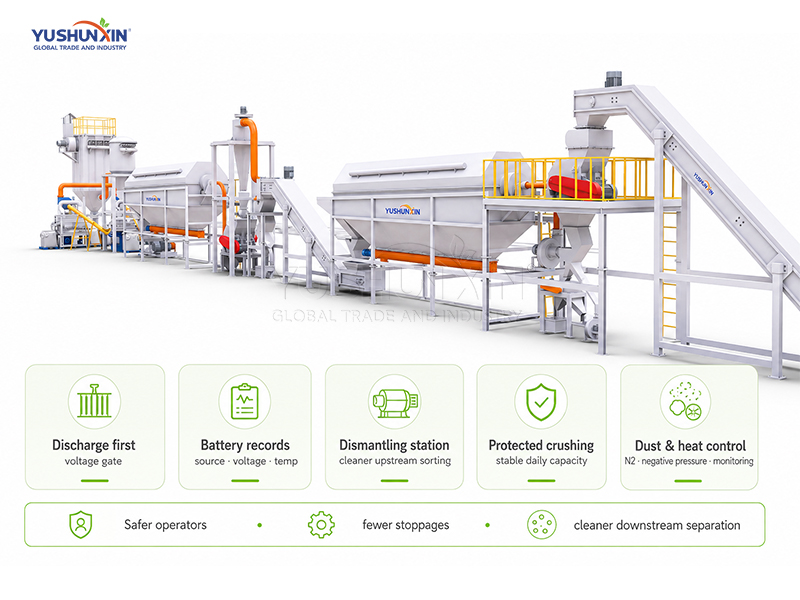
Discharge Sets The Entry Standard Before Pack Opening
Discharge should not work as an optional unit. It should become the first processing gate. Retired ESS packs and modules may still keep residual voltage. Поэтому, operators need voltage checking before dismantling. A better route connects testing, увольнять, batch records and material routing. Qualified batteries move to dismantling. Abnormal batteries return to the isolation area. The plant should record four key data points. These include battery source, Напряжение, temperature and discharge result. This record helps operators control safety responsibility.
Dismantling Stations Improve Safety And Downstream Stability
Protected Crushing Keeps Industrial Lines Running
How Can Operators Build a Multi-Output Recovery Plan?
05 · Recovery Plan
LFP battery recycling should not depend only on black mass value. Unlike high-nickel batteries, LFP packs need a broader recovery model. Поэтому, operators should set targets for черная месса, медь, алюминий, сталь, plastics and separator materials.
Define Output Targets Before Selection
Recovery targets determine equipment configuration. The line should balance black mass recovery, разделение металлов, purity control, and packaging requirements.
Match Separation With Buyer Standards
Magnetic, air, гравитационное разделение, and screening should follow product requirements. Controlling impurities, влага, and batch stability improves buyer acceptance.
Build Measurable Recovery Performance
A practical line should track black mass yield, восстановление металла, and material loss. Data helps optimize operation and improve long-term project returns.
How Can A Purchase Plan Prove Safety, Approval And Return?
06 · Purchase PlanA retired LFP battery project should not rely on machine price alone. Operators need to review safety design, approval documents, operating cost and recovery value. Поэтому, the purchase plan should prove both project feasibility and long-term return.
Project Documents Support Approval
Complete documents such as process flow, макет, electrical drawings, and manuals help reduce approval risks and support project review.
ROI Should Include Operating Costs
Project returns depend on recovery value, disposal costs, труд, обслуживание, and capacity. Accurate data helps select the right recycling solution.
Краткое содержание
Retired LFP battery disposal planning should connect safe storage, discharge control, pack dismantling, protected crushing, material separation and compliance documents. For energy storage operators, a complete solution can reduce project risk and improve recovery value. We can provide an industrial LFP battery recycling solution based on battery type, annual retirement volume and target outputs. We can also support related project needs, including ESS battery recycling plant, восстановление черной массы для переработки литиевых батарей, и lithium battery recycling plant cost.
Из ваших потребностей
к реальному воздействию


